Food Plant Hygiene Zones Need a Changeover Point, Not Just a Color Code
Food processing buyers specify color-coded workwear for raw, cooked, allergen, and packaging zones, then discover that cross-contamination still occurs at shift change and zone transitions. The root cause: color coding assumes workers change garments at a controlled point, but most plants have no designated changeover location with dirty and clean sides. The result: contaminated garments travel through shared corridors, break rooms, and stores, defeating the color-coding system. This article covers the changeover point design that makes color coding effective, the procurement specification for zone-specific garments, and the operational protocol that prevents cross-contamination at zone transitions.
Buyer context
What procurement teams run into
Food processing workwear presents a control gap that most buyers do not recognise until they see allergen cross-contamination or microbiological test failures traceable to garment movement between zones. The core issue: buyers specify color-coded workwear — white for raw meat, blue for cooked product, yellow for allergen handling, green for packaging — assuming that distinct colors prevent cross-contamination. But color coding only works if workers change garments at a controlled changeover point between zones. Most food plants do not have a designated changeover location with physical separation of dirty and clean sides. The result: workers finish a shift in a raw zone, walk through a shared corridor wearing the contaminated garment, collect personal items from a locker adjacent to the cooked zone, and start the next shift in the cooked zone — carrying pathogens on the garment surface across the hygiene boundary. **1. Color coding without changeover control is a visual system, not a hygiene system** Color-coded workwear is intended to create a visual barrier: workers and supervisors can immediately identify which zone a garment belongs to, and intervene if a worker enters the wrong zone wearing the wrong color. But the visual system only prevents wrong-zone entry during active work. It does not prevent cross-contamination during zone transitions: - **Shift change:** A worker finishes a shift in the raw zone, walks to the locker room wearing the contaminated garment, changes into personal clothing, and returns the next morning. The contaminated garment hangs in the locker overnight, shedding pathogens onto adjacent garments and locker surfaces. - **Break transitions:** A worker takes a break, walks to the break room wearing the zone garment, touches shared surfaces (tables, door handles, vending machines), and returns to a different zone after the break. - **Store and maintenance access:** A maintenance technician enters a raw zone to repair equipment, wearing the same garment used in the cooked zone earlier that day. The garment carries cooked-zone allergens into the raw zone, or raw-zone pathogens into the cooked zone. The color code is defeated because the garment moves between zones without a controlled changeover process. The visual system catches only the most obvious violations — it does not address the routine transitions where cross-contamination actually occurs. **2. The changeover point: physical separation of dirty and clean sides** The solution is a designated changeover point at each zone boundary, with physical separation of the dirty side (where contaminated garments are removed) and the clean side (where clean garments are collected). The changeover point design: - **Dirty side:** Located inside the zone boundary. The worker removes the contaminated garment and places it in a closed laundry bin or hook on the dirty side. The dirty side has floor drainage or non-porous flooring that can be cleaned and sanitised between shifts. - **Physical barrier:** A bench, step-over barrier, or partition separates the dirty side from the clean side. The worker cannot cross from the dirty side to the clean side without stepping over or around the barrier — forcing a conscious changeover action. - **Clean side:** Located outside the zone boundary. The worker collects a clean garment from a hook or dispenser on the clean side, and dresses before entering the next zone. The clean side is maintained at a higher hygiene standard (sanitised surfaces, positive air pressure if required). - **Hand hygiene:** A hand sanitiser station or sink is located at the changeover point, between removing the dirty garment and donning the clean garment. Hand hygiene is the most critical cross-contamination vector during changeover. The changeover point forces a controlled transition: the worker cannot move between zones without removing the contaminated garment, performing hand hygiene, and donning a clean garment. The physical barrier prevents the shortcut of walking through in the dirty garment. **3. The procurement mistake: specifying color coding without changeover infrastructure** The most common procurement error is to order color-coded garments without specifying or verifying that the plant has changeover infrastructure. The logic: "If we have four colors for four zones, workers will wear the right color in the right zone." But this logic assumes that workers change garments at the zone boundary — an assumption that fails when there is no designated changeover point. The buyer who specifies color coding without changeover infrastructure faces two risks: - **Cross-contamination:** Garments move between zones without controlled changeover, carrying pathogens or allergens across hygiene boundaries. Microbiological test failures or allergen recalls trace back to garment movement. - **Compliance failure:** Food safety auditors (BRC, SQF, FSSC 22000) require evidence of controlled garment changeover between hygiene zones. A plant with color-coded garments but no changeover points fails the audit finding for "inadequate control of clothing movement between zones." Neither outcome is acceptable. The buyer must specify changeover infrastructure as part of the workwear procurement scope — or verify that the plant has installed changeover points before committing to a color-coded garment order. **4. The garment specification for zone-specific workwear** The procurement specification for food processing workwear must address zone-specific requirements: - **Raw zone (raw meat, poultry, seafood):** Specify garments with smooth, non-absorbent fabric surfaces that do not retain moisture or pathogens. Polyester or polyester-blend fabrics with antimicrobial finish reduce bacterial retention. Garments must withstand high-temperature washing (70–80°C) with alkaline detergent for pathogen elimination. No external pockets below chest level (pockets collect drips and contaminants). - **Cooked zone (ready-to-eat, pasteurised product):** Specify garments in a distinct color (blue or green) with the same high-temperature wash durability as raw zone garments. The cooked zone garment must not be interchangeable with the raw zone garment — the color distinction must be enforced by separate laundry streams and separate storage. - **Allergen zone (nuts, dairy, soy, gluten):** Specify garments in a third distinct color (yellow or orange) with the same wash durability. The allergen zone garment must be washed in a dedicated cycle to prevent allergen cross-contamination — the buyer must specify separate laundry processing for allergen garments. - **Packaging zone (finished product, low-risk):** Specify garments in a fourth distinct color, or allow a lower-specification garment (lighter fabric weight, standard polyester) for low-risk packaging operations. The packaging zone garment does not require the same pathogen control as raw or cooked zones, but must still be visually distinct to prevent wrong-zone entry. **5. The laundry and storage protocol that supports color coding** Color-coded workwear requires a laundry and storage protocol that maintains zone separation: - **Separate laundry streams:** Raw zone, cooked zone, and allergen zone garments must be washed in separate loads — not mixed in the same wash cycle. Mixing raw and cooked garments in the same wash transfers pathogens from raw garments to cooked garments, defeating the color-coding system. The buyer must specify separate laundry processing as part of the workwear service contract. - **Separate storage:** Clean garments must be stored in zone-specific locations — separate hooks, dispensers, or lockers for each color. Mixed storage (all colors on the same rack) allows workers to pick up the wrong color, or to take a clean garment from the wrong zone in a rush. - **Garment tracking:** Use RFID tags or barcoded labels on each garment to track which zone the garment is assigned to, and whether it has been through the correct laundry cycle. Garment tracking provides audit evidence that color-coded garments are processed correctly — a requirement for BRC and SQF certification. **6. The pilot protocol for validating changeover effectiveness** Before committing to a color-coded workwear programme, pilot the changeover protocol with 5–10 workers per zone for 2–4 weeks: - **Changeover compliance:** Observe workers during zone transitions. Record whether workers use the changeover point, perform hand hygiene, and don the correct color garment before entering the next zone. If compliance is below 90%, investigate the root cause (changeover point location inconvenient, time pressure, lack of supervision) and adjust the protocol. - **Microbiological testing:** Swab garment surfaces at the end of each shift, before and after implementing the changeover protocol. Compare pathogen counts (total aerobic count, Enterobacteriaceae) on garments from workers who use the changeover point versus workers who do not. The pilot should demonstrate a measurable reduction in pathogen counts on garments after changeover protocol implementation. - **Audit readiness:** Document the changeover protocol, garment tracking data, and microbiological test results. Provide this documentation to the food safety auditor as evidence of controlled garment movement between zones.
Sourcing approach
How a factory partner can respond
The solution for food processing workwear is to pair color-coded garments with designated changeover points at each zone boundary, separate laundry streams for each zone, and a pilot protocol that validates changeover compliance before full fleet commitment. **Step 1: Install changeover points at each zone boundary** Design and install a changeover point at every transition between raw, cooked, allergen, and packaging zones. The changeover point must include: - **Dirty side:** Inside the zone boundary, with a closed laundry bin or hook for contaminated garments. Non-porous, drainable flooring. - **Physical barrier:** A bench, step-over partition, or swing gate that forces the worker to pause and change garments before crossing. - **Clean side:** Outside the zone boundary, with a hook or dispenser for the clean garment of the next zone's color. Sanitised surfaces. - **Hand hygiene:** A hand sanitiser station or sink between the dirty side and clean side. Verify that the changeover point is located on the direct route between zones — if workers must walk 50 metres out of their way to use the changeover point, they will skip it. **Step 2: Specify zone-specific garments in the procurement specification** Include the following requirements in the procurement specification: - **Raw zone:** Smooth, non-absorbent polyester or polyester-blend fabric, 180–220 GSM, with antimicrobial finish. Withstands 70–80°C washing. No external pockets below chest level. Color: white. - **Cooked zone:** Same fabric specification as raw zone. Color: blue or green (distinct from raw zone). - **Allergen zone:** Same fabric specification. Color: yellow or orange. Specify dedicated laundry cycle for allergen garments — allergen garments must not be washed in the same load as non-allergen garments. - **Packaging zone:** Lighter specification acceptable — 150–180 GSM polyester, standard wash durability. Color: fourth distinct color. **Step 3: Specify separate laundry streams and storage** Include the following requirements in the workwear service contract: - **Separate laundry loads:** Raw, cooked, and allergen garments must be washed in separate loads — never mixed. Specify wash temperature (70–80°C) and detergent type (alkaline, enzymatic for allergen removal). - **Separate storage:** Clean garments stored in zone-specific locations — separate hooks, dispensers, or lockers for each color. Mixed storage is not acceptable. - **Garment tracking:** RFID or barcode labels on each garment for zone assignment tracking and laundry cycle verification. Provide audit-ready data on garment movement and laundry compliance. **Step 4: Pilot the changeover protocol before full fleet commitment** Pilot the changeover protocol with 5–10 workers per zone for 2–4 weeks: - **Compliance observation:** Record whether workers use the changeover point, perform hand hygiene, and don the correct color garment. If compliance is below 90%, adjust the changeover point location, add signage, or assign a hygiene supervisor to monitor transitions. - **Microbiological testing:** Swab garments at shift end, before and after changeover implementation. Compare pathogen counts to demonstrate the changeover protocol's effectiveness. - **Audit documentation:** Document the protocol, compliance data, and test results. Provide to the food safety auditor as evidence of controlled garment movement. **Step 5: Adjust the programme based on pilot data** After the pilot, adjust the workwear programme: - **If changeover compliance is low:** Relocate the changeover point to a more convenient location, add visual cues (floor markings, signage), or assign a hygiene supervisor to monitor transitions during peak changeover times. - **If pathogen counts do not improve:** Investigate whether the laundry process is effective — swab garments after washing to confirm that the wash cycle eliminates pathogens. If not, increase wash temperature, change detergent, or extend wash cycle duration. - **If allergen cross-contamination persists:** Verify that allergen garments are washed in a dedicated cycle — if allergen garments are mixed with non-allergen garments in the same wash, allergen proteins transfer to non-allergen garments. Specify a separate wash cycle for allergen garments, and validate with allergen swab testing after washing. **Recommended garments for food processing workwear:** - **Industrial coverall-pro** — specify the 200–220 GSM polyester version with smooth, non-absorbent fabric surface and antimicrobial finish for raw and cooked zone workers. The coverall provides full-body coverage, withstands high-temperature washing (70–80°C), and has no external pockets below chest level to prevent drip collection. Specify the coverall in white for raw zones and blue or green for cooked zones, with separate laundry streams for each color. - **Logistics polo uniform** — specify the 150–180 GSM polyester version for packaging zone and warehouse workers in low-risk areas. The polo provides comfort and breathability for lighter-duty operations, and is visually distinct from raw and cooked zone garments. Specify the polo in a fourth distinct color (yellow or orange) for packaging zone identification.
Recommended Products
Products that fit this use case
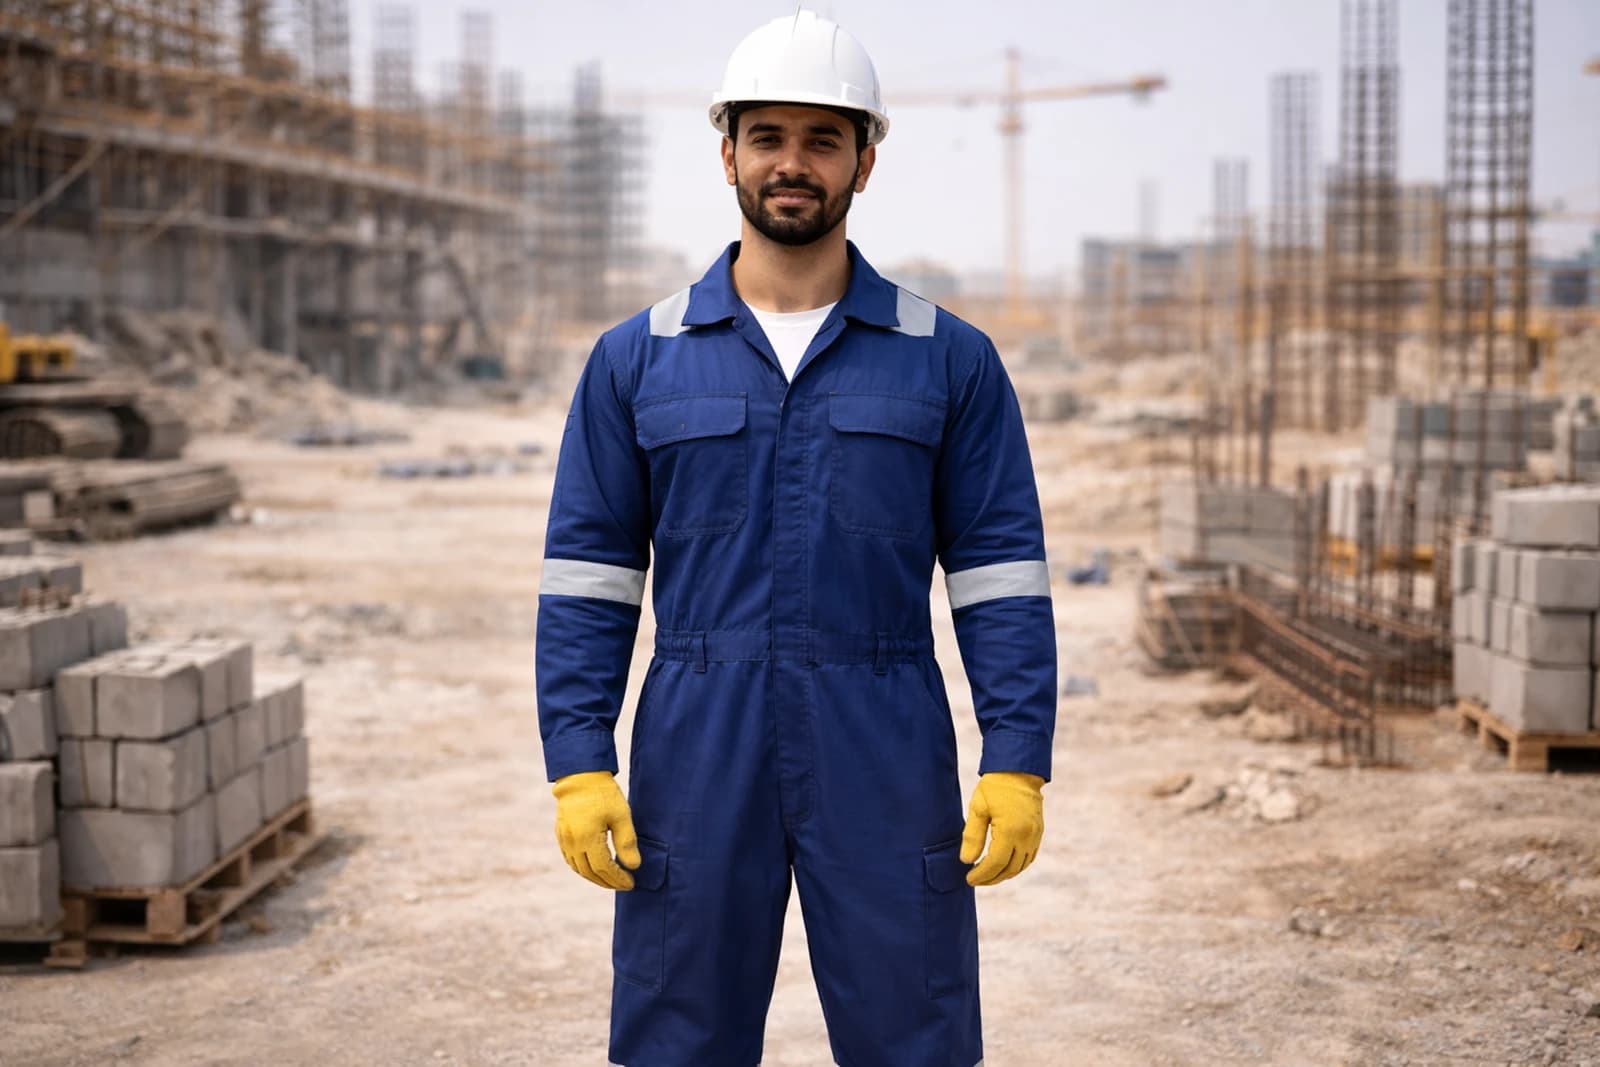
Industrial Workwear
Industrial Coverall Pro
Hard-wearing one-piece coverall for plant, maintenance, and heavy-duty operations.
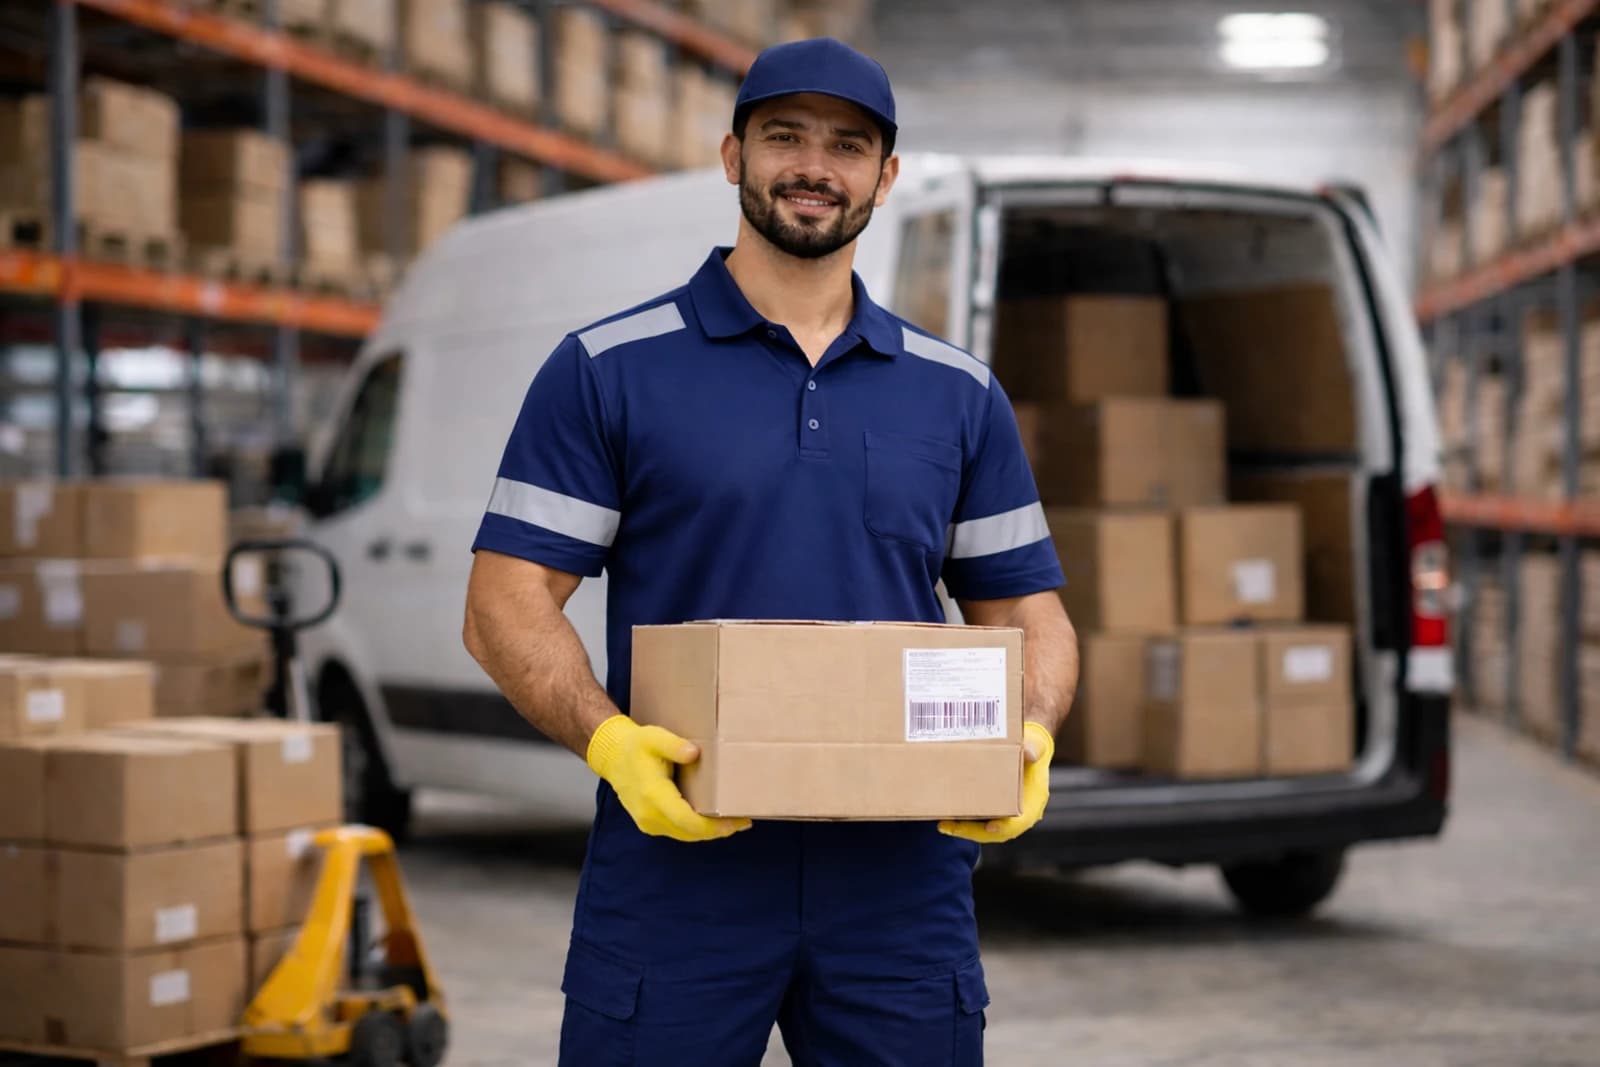
Logistics Uniform
Logistics Polo Uniform
Breathable uniform polo for warehouse, delivery, and last-mile teams.