H2S Corrodes Metal Zippers on Wastewater Workwear Before the Fabric Shows Any Wear
Wastewater treatment buyers specify chemical-resistant garments for hydrogen sulfide (H2S) environments, then discover that metal zippers, snaps, and D-rings corrode within weeks while the fabric remains intact. The root cause: H2S gas reacts with metal closures to form metal sulfides that weaken and embrittle the component, causing zipper teeth to separate, snaps to detach, and D-rings to fracture. The result: garments become unwearable not because the fabric failed, but because the metal closures corroded — creating a replacement cost that buyers did not anticipate. This article covers the H2S corrosion mechanism that destroys metal closures, the procurement specification for non-corrosive closures in wastewater workwear, and the inspection protocol that detects closure corrosion before garment failure.
Buyer context
What procurement teams run into
Wastewater treatment workwear presents a failure mode that most buyers do not recognise until they see garments with intact fabric but corroded, non-functional closures. The core issue: wastewater treatment facilities generate hydrogen sulfide (H2S) gas in headworks, screening areas, sludge handling zones, and anaerobic digesters. H2S is present at concentrations ranging from 1–100 ppm in enclosed areas and 0.5–10 ppm in open process areas. Buyers specify chemical-resistant garments — polyester or polyester-blend fabrics with chemical splash protection — assuming that the fabric's resistance to chemical degradation is the primary concern. But H2S gas does not just attack fabric; it attacks metal. And the metal components on workwear garments — zippers, snaps, D-rings, eyelets — are typically made from carbon steel, brass, or aluminium, all of which corrode rapidly in H2S environments. **1. Where H2S is generated in wastewater treatment** Hydrogen sulfide is produced by anaerobic bacteria that decompose organic matter in sewage. H2S is generated continuously in: - **Headworks and screening:** Raw sewage enters the plant through the headworks, where screens remove large debris. The turbulence and aeration of raw sewage releases H2S gas into the air. Enclosed headworks buildings accumulate H2S to concentrations of 10–50 ppm. - **Sludge handling:** Sludge thickeners, centrifuges, and sludge storage tanks produce H2S at concentrations of 50–200 ppm in enclosed areas. Workers who operate sludge equipment wear workwear garments exposed to high H2S concentrations. - **Anaerobic digesters:** Digesters produce biogas containing 1–5% H2S. Workers who perform maintenance on digester equipment, valves, and piping wear garments exposed to elevated H2S. - **Open process areas:** Aeration basins, clarifiers, and open channels release H2S at lower concentrations (0.5–5 ppm), but the continuous exposure over an 8-hour shift still corrodes metal closures. The worker's garment is exposed to H2S gas throughout the shift. The gas contacts the metal closures on the garment — zipper teeth, snap buttons, D-ring attachment points — and initiates a chemical reaction that corrodes the metal. **2. How H2S corrodes metal closures** H2S reacts with metal to form metal sulfides. The reaction depends on the metal type: - **Carbon steel:** H2S reacts with iron in carbon steel to form iron sulfide (FeS). Iron sulfide is a black, brittle compound that flakes off the metal surface, exposing fresh metal to further corrosion. Carbon steel zippers corrode visibly within 2–4 weeks of continuous H2S exposure. The zipper teeth become brittle, the zipper slider jams, and the zipper separates under normal use. - **Brass:** H2S reacts with copper and zinc in brass to form copper sulfide (Cu₂S) and zinc sulfide (ZnS). Brass corrodes more slowly than carbon steel, but brass snaps and eyelets still show visible corrosion (black or green discoloration) within 4–8 weeks of continuous H2S exposure. The snaps become difficult to fasten, and the eyelets weaken and crack. - **Aluminium:** H2S reacts with aluminium to form aluminium sulfide (Al₂S₃). Aluminium sulfide is a white, powdery compound that forms on the metal surface. Aluminium D-rings and adjustment hardware corrode within 3–6 weeks, losing structural strength and becoming brittle. The corrosion is progressive: the metal component does not fail suddenly, but degrades over weeks of exposure. The worker may not notice the corrosion until the zipper jams or the snap detaches during use. By that point, the garment is unwearable — not because the fabric failed, but because the closure failed. **3. Which garment components fail first** The metal components on workwear garments that are most vulnerable to H2S corrosion: - **Zippers:** The zipper teeth, slider, and stop are typically made from carbon steel or brass. The zipper is the most critical closure on a coverall — if the zipper fails, the garment cannot be worn. Zippers fail first because they have the largest metal surface area exposed to H2S, and the zipper teeth are thin (1–2 mm) and corrode through quickly. - **Snap buttons:** Snap buttons are typically made from brass or carbon steel with a plated finish. The plating (nickel, chrome, or zinc) provides temporary corrosion resistance, but the plating wears off at the contact point where the snap fastens and unfastens. Once the plating is worn, the base metal is exposed to H2S and corrodes. - **D-rings and attachment points:** D-rings are typically made from carbon steel or aluminium. D-rings are used for attaching lanyards, tools, or fall protection equipment. If the D-ring corrodes and fractures under load, the attached equipment falls — creating a safety hazard. - **Eyelets and grommets:** Eyelets are typically made from brass or carbon steel. Eyelets reinforce lace holes or ventilation openings. Corroded eyelets crack and tear the fabric around the eyelet, damaging the garment. The common failure sequence: zipper corrosion (2–4 weeks) → snap corrosion (4–8 weeks) → D-ring corrosion (6–10 weeks) → eyelet corrosion (8–12 weeks). The zipper fails first, rendering the garment unwearable, even though the fabric may have 6–12 months of service life remaining. **4. The procurement mistake: specifying fabric without specifying closures** The most common procurement error is to specify the garment fabric (polyester, chemical-resistant) without specifying the closure material. The logic: "If the fabric is chemical-resistant, the garment will withstand the H2S environment." But this logic ignores the fact that H2S corrodes metal, and the garment's metal closures are not chemical-resistant even if the fabric is. The buyer who specifies fabric without specifying closures faces two risks: - **Premature garment failure:** Metal closures corrode and fail within 2–8 weeks, while the fabric has 6–12 months of service life. The garment is discarded because the closure failed, wasting the remaining fabric life. The replacement cost is 4–6× higher than if the garment had been specified with non-corrosive closures. - **Safety hazard:** Corroded D-rings fracture under load, causing attached equipment (lanyards, tools) to fall. Corroded zippers jam or separate, exposing the worker to chemical splash or biological hazard. The closure failure creates a safety incident that is not obviously related to the garment specification. Neither outcome is acceptable. The buyer must specify closure material as part of the workwear procurement specification — not just fabric material. **5. The consequences of closure corrosion** The consequences of metal closure corrosion in wastewater workwear: - **Increased replacement cost:** Garments are discarded when closures fail, even though the fabric is intact. If a garment costs $40 and lasts 4 weeks due to zipper corrosion, the annual replacement cost per worker is $520 ($40 × 13 replacements). If the same garment is specified with a plastic zipper that lasts 6 months, the annual replacement cost drops to $80 ($40 × 2 replacements) — a 85% reduction. - **Worker downtime:** Workers spend time replacing garments when closures fail, reducing productive work time. A worker who spends 15 minutes replacing a garment with a failed zipper loses 15 minutes of productive work — multiplied across the workforce, this adds up to significant lost productivity. - **Safety incidents:** Corroded D-rings fracture under load, causing attached equipment to fall. A worker wearing a harness attached to a corroded D-ring on their workwear garment faces a fall hazard if the D-ring fractures. The safety incident is traceable to the garment specification that did not require non-corrosive D-rings.
Sourcing approach
How a factory partner can respond
The solution for wastewater treatment workwear is to specify non-corrosive closures (plastic zippers, plastic snaps, composite D-rings) as part of the garment procurement specification, implement an inspection protocol that detects closure corrosion before failure, and pilot garments with non-corrosive closures before full fleet commitment. **Step 1: Specify non-corrosive closures in the procurement specification** Include the following requirements in the procurement specification: - **Zippers:** Specify plastic zippers (polyacetal or nylon) with plastic sliders and stops. Plastic zippers do not corrode in H2S environments and maintain function for 6–12 months of continuous exposure. Specify zipper strength: the plastic zipper must withstand a minimum pull force of 80 N (newtons) to ensure that the zipper does not separate under normal use. Specify zipper color: black or dark grey to mask discoloration from H2S exposure (plastic zippers do not corrode, but may discolor from H2S gas contact). - **Snap buttons:** Specify plastic snaps (polyacetal or nylon) with plastic sockets and studs. Plastic snaps do not corrode and maintain fastening strength for 6–12 months. Specify snap strength: the plastic snap must withstand a minimum pull force of 50 N to ensure that the snap does not detach under normal use. - **D-rings and attachment points:** Specify composite D-rings made from glass-filled nylon or polypropylene. Composite D-rings do not corrode and maintain structural strength for 12–24 months. Specify D-ring load rating: the composite D-ring must withstand a minimum static load of 5 kN (kilonewtons) for fall protection attachment points, or 2 kN for tool attachment points. - **Eyelets and grommets:** Specify plastic eyelets (polyacetal or nylon) or stainless steel (316 grade) eyelets. Stainless steel 316 contains molybdenum, which resists H2S corrosion. Plastic eyelets do not corrode and are preferred for non-load-bearing applications (ventilation openings, lace holes). **Step 2: Specify closure inspection in the garment care protocol** Include the following inspection requirements in the workwear service contract: - **Weekly visual inspection:** Workers inspect garment closures weekly for signs of corrosion, discoloration, or stiffness. For metal closures: look for black or green discoloration (metal sulfide formation), white powder (aluminium sulfide), or stiffness when operating the zipper or snap. For plastic closures: look for cracks, discoloration, or deformation. - **Monthly functional test:** Workers operate each closure (zipper, snap, D-ring) monthly to confirm that it functions smoothly. A zipper that jams or requires excessive force to operate indicates corrosion or debris accumulation. A snap that does not fasten securely indicates corrosion or deformation. A D-ring that shows cracks or deformation must be replaced immediately. - **Closure replacement criteria:** Specify that garments with corroded or non-functional closures must be removed from service and replaced — even if the fabric is intact. Do not attempt to repair corroded metal closures; replace the garment. **Step 3: Pilot garments with non-corrosive closures before full fleet commitment** Before committing to a full fleet order, pilot garments with non-corrosive closures with 5–10 workers in the highest-H2S areas (headworks, sludge handling, digesters) for 8–12 weeks: - **Closure function monitoring:** Inspect garment closures weekly during the pilot. Record whether plastic zippers, snaps, and D-rings maintain function over the pilot period. Compare closure function against garments with metal closures worn by workers in the same areas. - **Worker feedback:** Survey workers on ease of use, comfort, and durability of plastic closures. Plastic zippers may feel different from metal zippers (lighter pull, different sound); confirm that workers adapt to the difference. If workers report that plastic snaps are difficult to fasten with gloved hands, specify larger-diameter snaps or snaps with a textured surface for better grip. - **Cost comparison:** Calculate the garment replacement cost during the pilot period for garments with plastic closures versus metal closures. The pilot should demonstrate that plastic closures extend garment life by 3–6×, reducing annual replacement cost per worker. **Step 4: Adjust the specification based on pilot data** After the pilot, adjust the garment specification: - **If plastic zippers jam or stick:** Investigate whether debris (flour, dust, dried sludge) is accumulating in the zipper teeth. Specify a zipper with a larger tooth gap to reduce debris accumulation, or specify a zipper cover flap to protect the zipper from debris. - **If plastic snaps detach:** Investigate whether the snap is being subjected to excessive force (workers pulling the snap apart at an angle rather than straight). Specify a larger-diameter snap or a snap with a higher pull-force rating. - **If composite D-rings crack:** Investigate whether the D-ring is being subjected to dynamic loading (shock loads from falling tools) rather than static loading. Specify a D-ring with a higher dynamic load rating, or specify a metal D-ring made from stainless steel 316 for high-load applications. **Recommended garments for wastewater treatment workwear:** - **Industrial coverall-pro** — specify the 200–220 GSM polyester version with plastic zipper (polyacetal), plastic snaps, and composite D-rings for workers in headworks, sludge handling, and digester areas where H2S concentrations are highest. The coverall provides full-body protection against chemical splash and biological hazard, with non-corrosive closures that withstand continuous H2S exposure for 6–12 months. Specify the coverall with sealed seams to prevent H2S gas penetration through needle holes, and with hi-vis retroreflective tape for workers who operate near vehicles or moving equipment. - **Hi-vis safety jacket** — specify the 200 GSM polyester version with plastic zipper and composite D-rings for workers in open process areas (aeration basins, clarifiers) where H2S concentrations are lower but visibility near vehicles and moving equipment is required. The hi-vis jacket provides visibility for roadside and forklift safety, with non-corrosive closures that withstand continuous low-level H2S exposure. Specify the hi-vis jacket as an outer layer worn over the coverall for workers who move between enclosed high-H2S areas and open process areas.
Recommended Products
Products that fit this use case
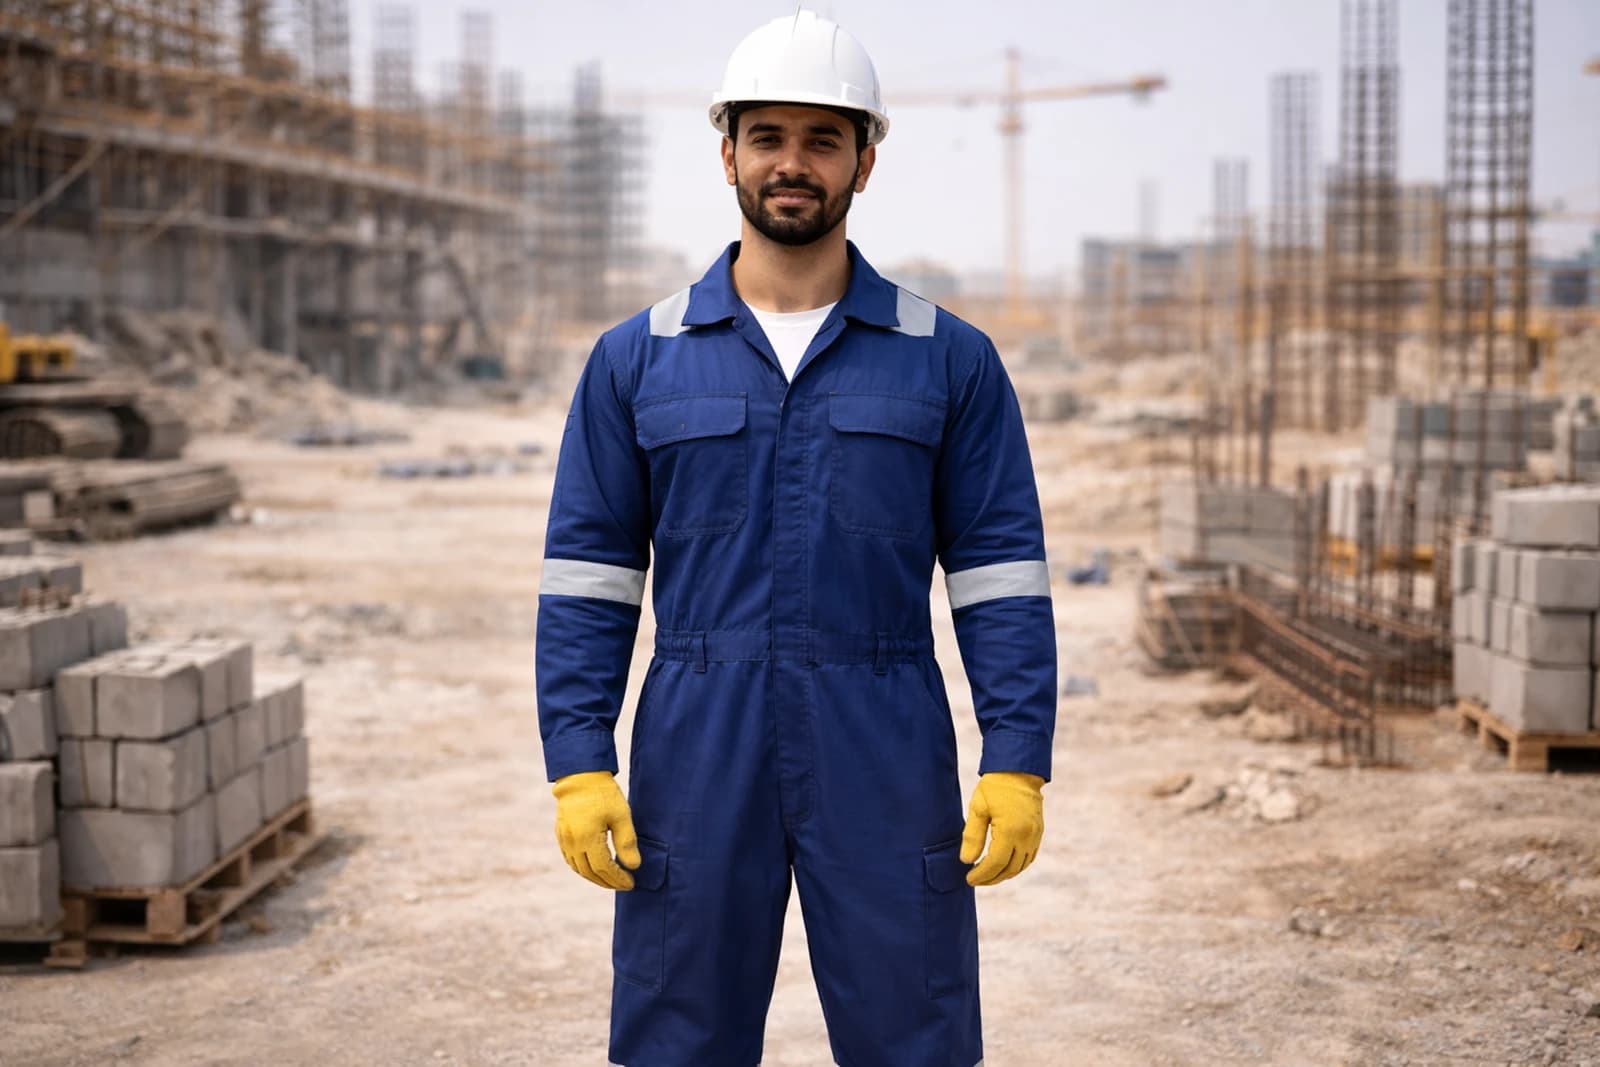
Industrial Workwear
Industrial Coverall Pro
Hard-wearing one-piece coverall for plant, maintenance, and heavy-duty operations.
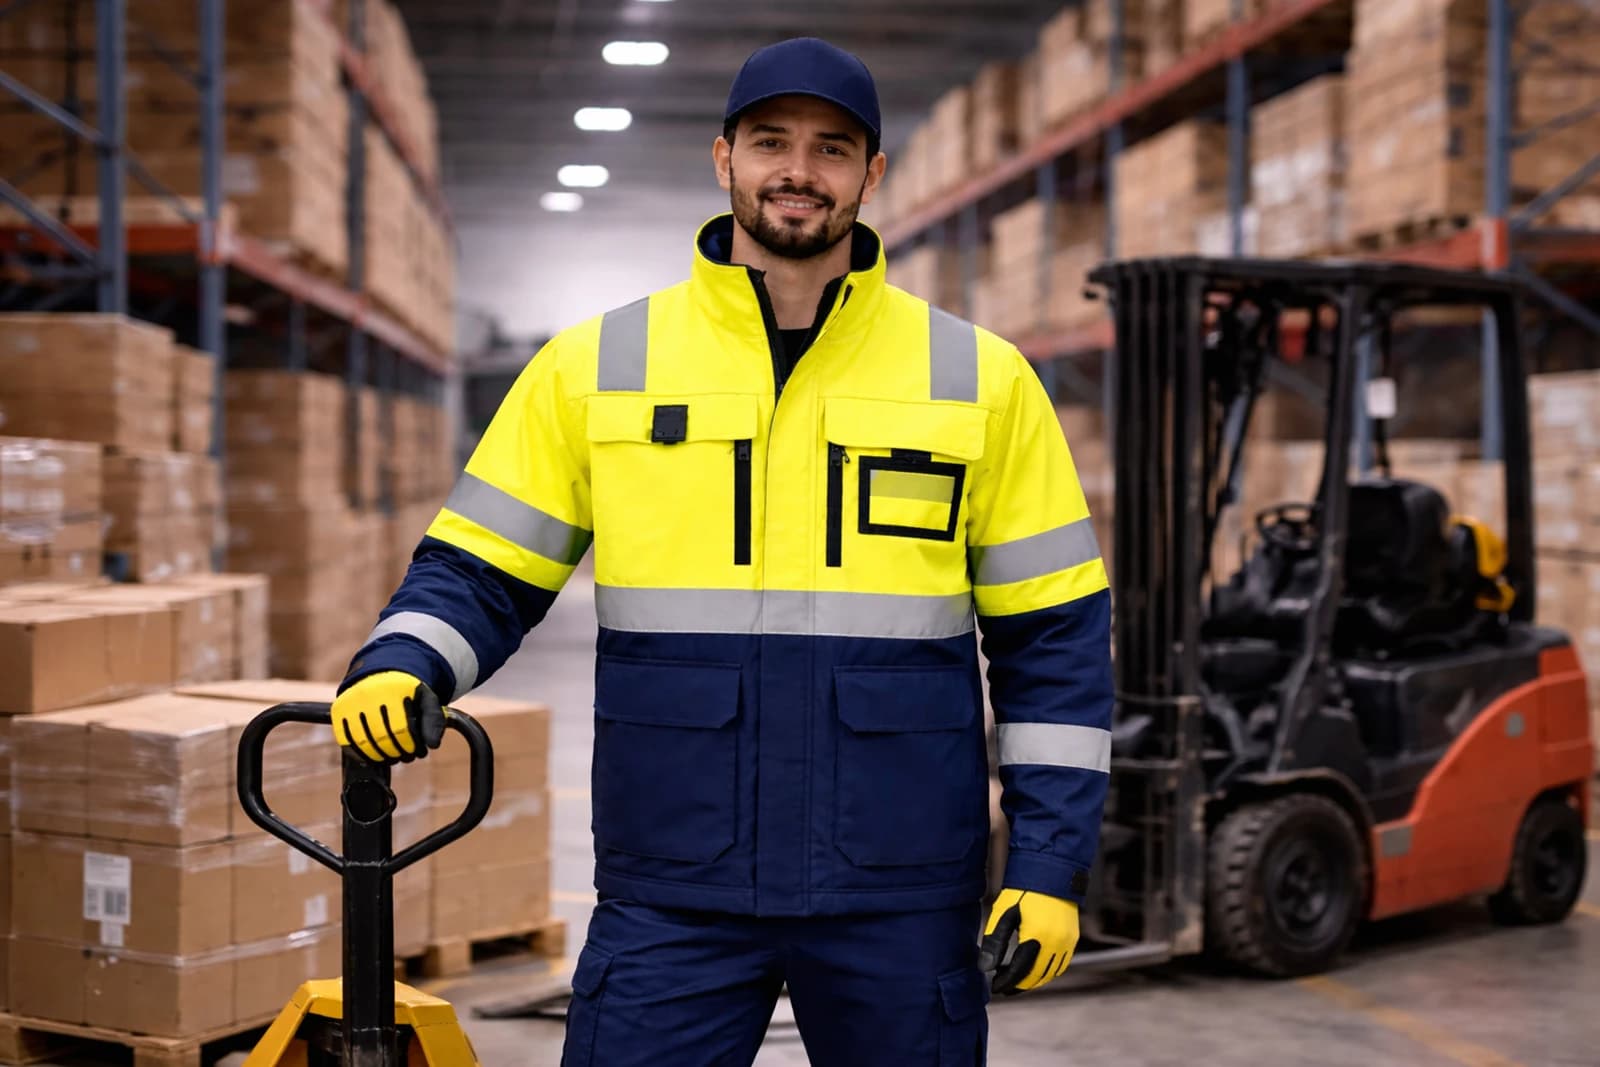
Safety Uniform
Hi-Vis Safety Jacket
Reflective safety jacket for high-visibility site operations and road work crews.