Incoming Workwear QA: Lot Acceptance Sampling Versus Single-Piece Inspection
Buyers who check one garment per shipment miss the real defect rate. Buyers who check every garment spend more on inspection than the defects are worth. Lot acceptance sampling gives a statistical answer — a defined sample size, a defect count threshold, and a clear accept-or-return decision — without inspecting every carton. This article covers how quality varies within a single workwear shipment, why single-piece checks fail, and how to set AQL levels and sample sizes for practical incoming inspection.
Buyer context
What procurement teams run into
Workwear buyers receiving shipment deliveries face an incoming quality control problem: how to verify that the shipment meets specification without inspecting every garment. Two common approaches fail in different ways. The first approach — pulling one or two garments from the shipment, checking them, and accepting the entire lot if those samples pass — misses quality variation across the shipment and lets defective garments reach workers. The second approach — checking every garment in the shipment — costs more in inspection labor and time than the defects themselves are worth, especially for large orders of 2,000–10,000 garments. Neither approach gives the buyer a defensible, repeatable quality decision. The mechanism: **1. Quality varies within a single workwear shipment across production lines, fabric rolls, and sewing teams** A single workwear shipment of 5,000 garments is not a uniform product. The shipment contains garments produced across multiple production days (potentially 5–15 production days), multiple sewing lines (2–6 lines in a typical factory), multiple fabric rolls (each roll producing 80–200 garments), and multiple sewing teams (each team with different skill levels). Quality variation exists across all of these dimensions: fabric shade varies between rolls, stitch tension varies between sewing lines, seam allowance varies between operators, and closure attachment (zippers, snaps, velcro) varies between production days. The root cause: workwear manufacturing is a batch process with multiple sources of variation. Even when a factory follows the same specification and the same production instructions, variation exists between fabric rolls (dye lot shade differences), between sewing operators (stitch density, seam alignment), and between production days (machine calibration drift, thread tension changes). A shipment of 5,000 garments may contain 3,000 garments that are perfectly within specification and 2,000 garments that have minor or major defects — and those defective garments are distributed across the shipment, not concentrated in one carton. **2. Single-piece inspection misses the defect distribution across the shipment** A buyer who pulls one carton from the shipment, opens it, checks two garments, and accepts the lot based on those two garments has no statistical basis for the acceptance decision. Two garments from one carton represent 0.04% of a 5,000-garment lot. The sample is too small to detect a 5% defect rate (250 defective garments) or even a 20% defect rate (1,000 defective garments). The probability that both sample garments are defect-free when the lot has a 20% defect rate is 64% — meaning the buyer accepts a lot with 1,000 defective garments two-thirds of the time. The root cause: single-piece or small-sample inspection does not account for lot variation. Defective garments are distributed across the shipment — some cartons contain more defects than others. A single-carton sample may come from a production run that happened to be well-controlled, while other cartons from different production runs contain defects. The buyer's sample is not representative of the lot. **3. Full-piece inspection costs more than the defects it catches** A buyer who decides to check every garment in a 5,000-piece shipment faces inspection costs that exceed the value of defects caught. Inspecting one garment — checking seams, closures, measurements, fabric, stitching, and appearance — takes 3–5 minutes per garment. Inspecting 5,000 garments takes 250–417 labor hours (31–52 work days for one inspector). The cost of inspection labor, facility time, and shipment delay exceeds the cost of the defects that would be caught. Additionally, full inspection creates its own quality problems: garments handled repeatedly during inspection develop handling damage (soiling, creasing, snagging) that was not present when the garments were packed. The root cause: full-piece inspection is economically irrational for workwear with a typical defect rate of 2–5%. The cost of finding and removing 100–250 defective garments (250–417 hours of inspection labor) exceeds the cost of replacing those garments through a supplier return or allowance. The buyer spends more on inspection than the defects are worth. **4. Without a defined sampling plan, the buyer has no defensible accept-or-return criterion** When a buyer inspects a sample of garments and finds defects, the decision to accept or return the shipment is subjective. The buyer has no predefined threshold: how many defects in the sample justify returning the entire shipment? Is one major defect enough? Three minor defects? Five? Without a predefined sampling plan with acceptance numbers, the buyer makes accept-or-return decisions based on instinct, relationship with the supplier, or pressure to get garments to workers — not based on a statistical quality criterion. The root cause: the buyer has not defined an acceptable quality level (AQL) — the maximum defect rate that the buyer is willing to accept — and has not defined a sampling plan that gives a statistical probability of accepting lots at or below the AQL and rejecting lots above the AQL. Without an AQL and a sampling plan, every inspection decision is ad hoc and indefensible. **5. Defect classification is not defined, so minor and major defects are weighted equally** Workwear defects vary in severity. A broken zipper on a coverall is a critical defect — the garment cannot be used. A stitch density that is 5% below specification is a minor defect — the garment is functional but does not meet spec. A fabric shade that is slightly off from the approved sample is a major defect — the garment is functional and durable but does not match the approved appearance. Without defect classification (critical, major, minor), the buyer treats all defects as equal and cannot set appropriate acceptance numbers for each defect category. The root cause: the buyer has not defined a defect classification list that categorizes defects by severity and sets different acceptance numbers for each category. Critical defects (garment cannot be used) have an acceptance number of zero — any critical defect in the sample triggers lot rejection. Major defects (garment function is affected or appearance does not match approval) have a low acceptance number. Minor defects (garment is functional and durable but has a cosmetic issue) have a higher acceptance number. **6. The cost of getting it wrong** The buyer who uses single-piece inspection faces: - Defective garments reaching workers (broken closures, open seams, incorrect sizing) - Worker complaints and replacement requests (workers receiving garments that fail within first wear) - Reputation loss with workers (workers losing confidence in the procurement process) - No statistical basis for supplier quality discussions (the buyer cannot quantify the defect rate) The buyer who uses full-piece inspection faces: - Inspection costs exceeding defect costs (labor and time spent inspecting every garment) - Shipment delays (inspection taking weeks, delaying garment distribution to workers) - Handling damage (garments damaged during inspection process) - No statistical basis for supplier quality discussions (the buyer has inspected every garment but has not established a repeatable sampling protocol for future shipments) The buyer who uses lot acceptance sampling faces: - Statistical confidence in the accept-or-return decision (the sampling plan gives a defined probability of accepting lots at or below AQL) - Inspection costs proportional to the risk (sample size is based on lot size and AQL, not full-piece inspection) - Defensible supplier quality discussions (the buyer can quantify defect rates and hold suppliers accountable to AQL standards) - Repeatable inspection protocol (the same sampling plan is used for every shipment, creating consistency)
Sourcing approach
How a factory partner can respond
The solution is a lot acceptance sampling plan for incoming workwear inspection — a statistical protocol that defines sample size, defect classification, and acceptance numbers for each shipment, giving the buyer a defensible accept-or-return decision without inspecting every garment. **Step 1: Define defect classification for workwear garments** Create a defect classification list that categorizes workwear defects into three severity levels: - **Critical defects:** defects that make the garment unusable or unsafe. Examples: broken zipper, missing closures, open seams that compromise garment integrity, incorrect fabric (fabric does not match specification — e.g., specified fabric weight is 240 gsm but actual fabric is 180 gsm), hi-vis retroreflective tape missing or non-compliant, FR garment without required FR treatment. Acceptance number for critical defects: zero. Any critical defect in the sample triggers lot rejection. - **Major defects:** defects that affect garment function or appearance significantly. Examples: seam stitch density below specification (e.g., specified 8–10 stitches per inch, actual 5–6 stitches per inch), fabric shade variation beyond approved tolerance (shade difference visible when compared to approved sample), incorrect sizing (garment measurements outside specification tolerance), misaligned closures (zipper or snap not aligned correctly), visible fabric defects (slubs, holes, weaving defects larger than 10mm). Acceptance number for major defects: set based on AQL (Step 2). - **Minor defects:** defects that are cosmetic and do not affect garment function or durability. Examples: loose thread ends (not trimmed), minor packaging defects (carton labeling incorrect, polybag torn), slight fabric shade variation within tolerance but not matching approved sample exactly, minor stitching irregularities that do not affect seam strength. Acceptance number for minor defects: set based on AQL (Step 2). The defect classification list ensures that inspection focuses on defect severity and that acceptance numbers are appropriate for each defect category. **Step 2: Set acceptable quality level (AQL) for each defect category** Set AQL levels for each defect category based on the consequence of defects reaching workers: - **Critical defects AQL: 0%** — no critical defects are acceptable. Any critical defect in the sample triggers lot rejection or 100% inspection for that defect. - **Major defects AQL: 2.5%** — the buyer accepts lots with up to 2.5% major defects. This AQL is appropriate for defects that affect garment function or appearance but do not create safety risk. - **Minor defects AQL: 4.0%** — the buyer accepts lots with up to 4.0% minor defects. This AQL is appropriate for cosmetic defects that do not affect garment function. The AQL levels define the maximum defect rate that the buyer is willing to accept. The sampling plan (Step 3) is designed to give a high probability of accepting lots at or below the AQL and a low probability of accepting lots above the AQL. **Step 3: Determine sample size using ISO 2859-1 (ANSI/ASQ Z1.4) sampling tables** Use ISO 2859-1 (or ANSI/ASQ Z1.4) sampling tables to determine the sample size for each shipment based on lot size and inspection level: - **Lot size:** the total number of garments in the shipment (e.g., 5,000 garments). - **Inspection level:** use General Inspection Level II for normal inspection. This level gives a balanced sample size that is neither too small (missing defects) nor too large (excessive inspection cost). - **Sample size code letter:** for a lot size of 5,000 garments at General Inspection Level II, the sample size code letter is L. The sample size for code letter L is 200 garments. The sampling table gives the sample size (200 garments from a lot of 5,000) and the acceptance numbers for each AQL level: - Critical defects AQL 0%: acceptance number 0, rejection number 1 - Major defects AQL 2.5%: acceptance number 10, rejection number 11 - Minor defects AQL 4.0%: acceptance number 14, rejection number 15 The buyer inspects 200 garments from the shipment and counts the number of critical, major, and minor defects. If critical defects > 0, reject the lot. If major defects > 10, reject the lot. If minor defects > 14, reject the lot. If all defect counts are at or below acceptance numbers, accept the lot. **Step 4: Select samples randomly from across the shipment** The 200 garments must be selected randomly from across the shipment — not from one carton, not from the top of the pallet, not from the most accessible cartons. Random selection ensures that the sample represents the entire lot, including garments from different production days, different sewing lines, and different fabric rolls. Random selection method: - Number every carton in the shipment (carton 1 to carton N). - Use a random number generator to select carton numbers proportional to the sample size. For a shipment of 500 cartons and a sample of 200 garments, select 100 cartons randomly and pull 2 garments from each selected carton. - Alternatively, select garments at random from the shipment by opening cartons at random locations (top, middle, bottom of pallet; front, middle, back of container). The random selection ensures that the sample represents the lot and that the inspection result is statistically valid. **Step 5: Inspect samples against the specification and defect classification list** Inspect each of the 200 sample garments against the approved specification and the defect classification list (Step 1). Check the following: - **Fabric:** fabric weight (gsm), fabric composition, fabric shade (compare to approved sample), fabric defects (slubs, holes, weaving defects). - **Construction:** seam stitch density (stitches per inch), seam allowance, seam strength (pull test), seam alignment. - **Closures:** zipper function (open and close smoothly), snap attachment (pull test), velcro adhesion (peel test), button attachment (pull test). - **Measurements:** garment dimensions (chest, waist, inseam, sleeve length, body length) compared to specification tolerance. - **Appearance:** overall appearance, color consistency, print or embroidery quality, labeling accuracy. - **Function:** hi-vis retroreflective tape presence and placement, FR treatment verification, water-repellent treatment verification. Record each defect found, categorized as critical, major, or minor. Count the total number of defects in each category. **Step 6: Make the accept-or-return decision based on acceptance numbers** Compare the defect counts to the acceptance numbers (Step 3): - If critical defects found > 0: reject the lot. Return the shipment to the supplier or require the supplier to perform 100% inspection and replacement of critical defects at supplier cost. - If major defects found > acceptance number (10 for AQL 2.5%, sample size 200): reject the lot. Return the shipment or negotiate a price allowance for the defect rate. - If minor defects found > acceptance number (14 for AQL 4.0%, sample size 200): reject the lot or accept with a price allowance for the minor defect rate. - If all defect counts are at or below acceptance numbers: accept the lot. Distribute garments to workers. Document the inspection result: sample size, defect counts by category, accept-or-return decision, and inspector name. Share the inspection report with the supplier to support quality improvement discussions. **Step 7: Track supplier quality performance across shipments** Record inspection results for every shipment from every supplier. Track the defect rate (critical, major, minor) for each shipment and calculate the supplier's average defect rate across shipments. Use the tracking data to: - Identify suppliers with consistently high defect rates (requiring corrective action or supplier replacement) - Identify suppliers with improving defect rates (indicating quality improvement investments) - Adjust AQL levels based on supplier performance (tighten AQL for suppliers with high defect rates, relax AQL for suppliers with consistently low defect rates) - Support supplier negotiations with objective quality data (the buyer can quantify the defect rate and hold suppliers accountable) The tracking data creates a feedback loop that improves supplier quality over time and gives the buyer objective data for supplier management. **Recommended garments for incoming QA inspection:** - **Industrial coverall-pro** — the coverall has multiple construction elements that require inspection: front zipper function, snap or velcro closure attachment, seam stitch density at torso, arms, and crotch seams, pocket placement and attachment, reflective tape presence and placement, and fabric weight and composition. The coverall's construction complexity means that defect classification (Step 1) should include critical defects (broken zipper, missing snap, open seam at crotch or torso), major defects (stitch density below specification, fabric shade variation, incorrect sizing), and minor defects (loose thread ends, minor packaging defects). The coverall's full-body coverage and multiple closure points make it a garment where incoming inspection catches defects that would otherwise reach workers and create functional failures. - **Logistics polo uniform** — the polo uniform has simpler construction than the coverall but still requires inspection: collar attachment, sleeve hem stitching, side seam strength, placket closure (buttons or snaps), print or embroidery quality (logo, worker name, company name), and fabric composition and weight. The polo uniform's simpler construction means that major defects are fewer (collar detachment, incorrect sizing, fabric shade variation) and minor defects are more common (loose thread ends, minor print irregularities). The polo uniform is a garment where incoming inspection focuses on appearance and labeling accuracy — defects that affect professional appearance and worker identification.
Recommended Products
Products that fit this use case
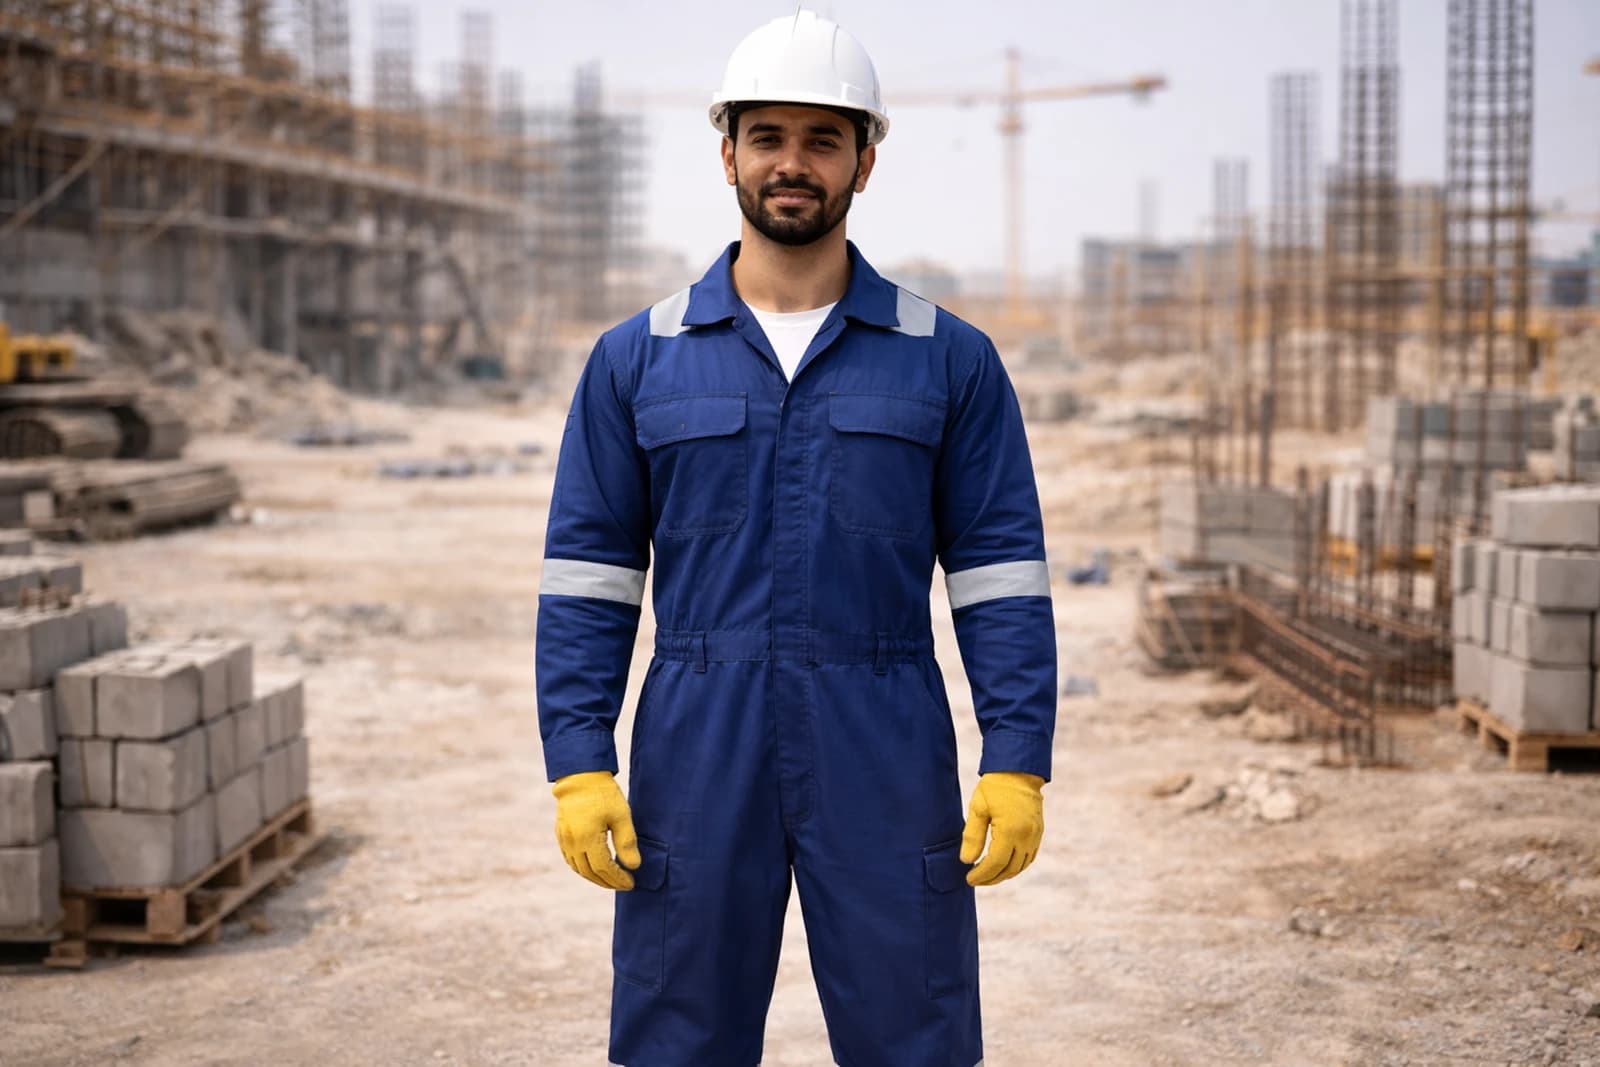
Industrial Workwear
Industrial Coverall Pro
Hard-wearing one-piece coverall for plant, maintenance, and heavy-duty operations.
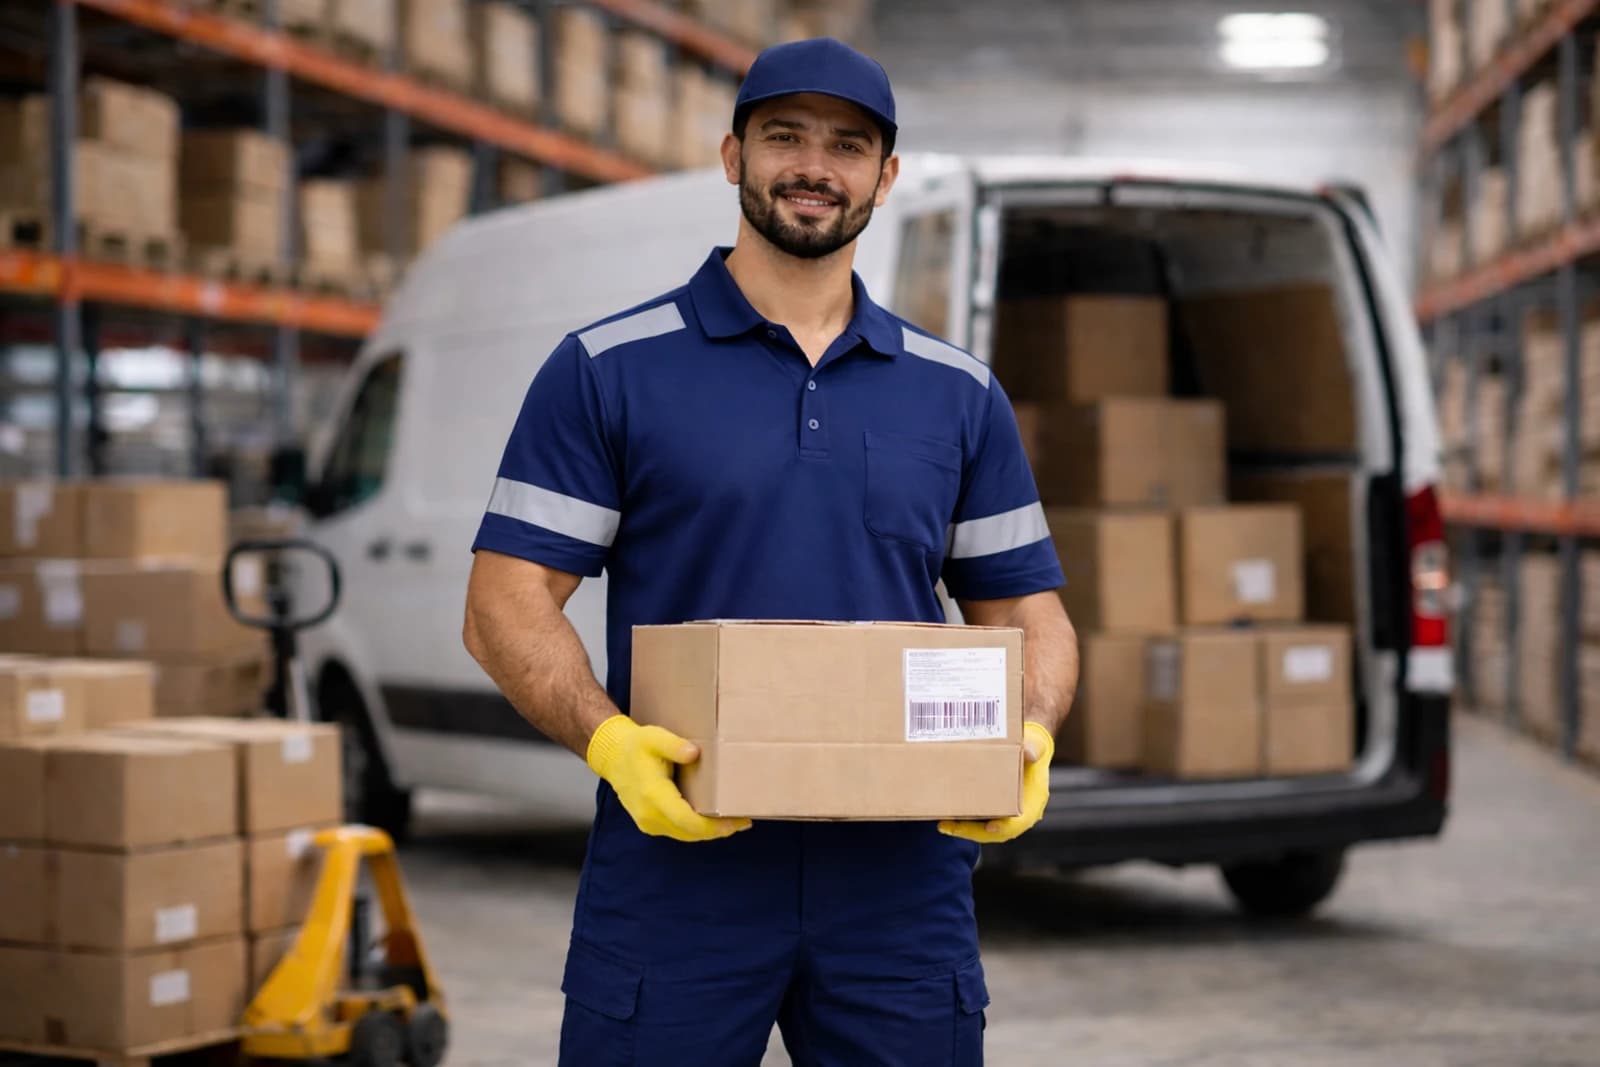
Logistics Uniform
Logistics Polo Uniform
Breathable uniform polo for warehouse, delivery, and last-mile teams.