What Workwear Constraints Matter Most in Automotive Paint Operations?
Automotive paint shops expose workers to solvents, paints, and coatings that penetrate standard workwear fabrics. Most specifications treat chemical exposure as a PPE glove problem — but workwear fabric absorbs and holds chemicals against skin throughout the shift, creating dermal exposure risk that gloves alone don't address. Paint shop workwear must also avoid contaminating the paint finish: lint, fibers, and particles shed from garments create paint defects that require costly rework. This article covers the fabric selection criteria that minimize chemical absorption and lint generation, the zone-based specification that matches garment coverage to each area's exposure level, and the laundering validation program that proves garments can be effectively decontaminated without degrading fabric properties.
Buyer context
What procurement teams run into
Automotive paint shops operate under a dual constraint that most workwear specifications don't address: workers face continuous chemical exposure from solvents, paints, and coatings, while garments must not contaminate the paint finish with lint, fibers, or particles. Standard workwear fabrics absorb chemicals and hold them against skin — creating dermal exposure risk — while also shedding particles that create paint defects requiring costly rework. The mechanism: **1. Standard workwear fabrics absorb and hold chemicals against skin** Cotton and cotton-blend fabrics — the default choice for general workwear — absorb solvents, paints, and coatings through capillary action. Once absorbed, chemicals are held in fabric fibers and released slowly through body heat and movement, creating continuous dermal exposure throughout the shift. Chemical exposure in automotive paint shops includes: - **Solvents:** thinners, reducers, and cleaners (toluene, xylene, acetone, methyl ethyl ketone) that dissolve paint and clean equipment. Solvents penetrate skin and enter bloodstream, causing neurological effects with chronic exposure. - **Paint resins and hardeners:** epoxy, polyurethane, and acrylic resins that contain isocyanates, amines, and other reactive chemicals. Isocyanates are potent sensitizers — skin exposure can cause occupational asthma and dermatitis. - **Pigments and additives:** metal-based pigments (chromium, lead in older formulations), UV stabilizers, and flow agents that may contain hazardous substances. The root cause: standard workwear fabrics are not designed for chemical resistance. Absorbent fabrics hold chemicals against skin, creating dermal exposure that gloves alone don't address. **2. Garment lint and fiber shedding create paint defects** Automotive paint finishes require flawless surfaces — a single lint particle or fiber embedded in wet paint creates a defect that requires sanding, repainting, and polishing. Paint defects are costly: rework requires stripping the panel, repriming, repainting, and clear-coating — adding 2-4 hours of labor per defect. Standard workwear fabrics shed fibers and particles through: - **Movement and abrasion:** workers reaching, bending, and walking generate friction that releases fibers from fabric surface - **Washing degradation:** repeated industrial laundering breaks down fabric fibers, increasing lint generation over time. After 25-50 wash cycles, fabric may shed significantly more lint than at receipt. - **Fabric surface texture:** brushed cotton, fleece-lined fabrics, and textured surfaces create loose fibers that release easily. Loose fibers become airborne and settle on wet paint surfaces. The root cause: standard workwear fabrics are not designed for low-lint performance. Fabrics that shed lint create paint defects that require costly rework. **3. Workers move between zones with different exposure levels** Automotive paint shops have distinct zones with different chemical exposure and contamination control requirements: - **Paint mixing and preparation areas:** workers handle concentrated solvents, paints, and hardeners. Chemical exposure is highest here — workers contact undiluted chemicals during mixing, thinning, and equipment cleaning. - **Paint application (spray booths):** workers apply paint to vehicle bodies. Chemical exposure is high (spray mist, overspray) and contamination control is critical (garment lint can defect wet paint). - **Curing and inspection areas:** painted vehicles move through curing ovens and inspection stations. Chemical exposure is lower (paint is curing or cured), but contamination control remains important (lint can still defect surfaces during inspection). - **Administrative and support areas:** minimal chemical exposure and contamination control requirements. Workers move between zones throughout the shift — from mixing to spray booth to inspection. A worker wearing chemically contaminated workwear in the mixing area carries that contamination into spray booths and inspection areas. The garment becomes a chemical transport vector — moving chemicals from high-exposure areas into areas where contamination should be controlled. The root cause: workwear that absorbs chemicals in high-exposure areas becomes a mobile contamination source that spreads chemicals across facility zones, undermining contamination control in paint application and inspection areas. **4. Frequent laundering is required but degrades garments not specified for wash durability** Paint shop workwear requires frequent laundering to remove chemical residues and maintain low-lint performance. Daily or shift-change laundering is necessary to prevent chemical buildup and lint generation. Industrial laundering degrades garments: - **Fabric breakdown:** washing breaks down fabric fibers, increasing lint generation and chemical absorption over time. After 25-50 wash cycles, fabric may generate more lint and absorb more chemicals than at receipt. - **Chemical resistance degradation:** chemical-resistant treatments (water-repellent finishes, chemical-barrier coatings) degrade through washing. Garments that resist chemical absorption at receipt may not resist absorption after 10-25 wash cycles. - **Seam and closure degradation:** washing degrades seams and closures, creating additional lint generation points and reducing garment integrity. The root cause: without wash durability validation, buyers cannot prove that garments maintain chemical resistance and low-lint performance throughout their service life. A garment that performs well at receipt may generate more lint and absorb more chemicals after 25 wash cycles. **5. The cost of getting it wrong** The buyer who specifies standard workwear for automotive paint shops without addressing chemical absorption and lint generation faces: - Chronic chemical exposure for workers (dermal contact with solvents, isocyanates, pigments) - Paint defects requiring costly rework (lint particles embedded in wet paint) - Regulatory liability (occupational health violations from chemical exposure) - Budget waste (replacing garments that degrade prematurely, under-replacing garments that absorb chemicals or generate lint) The buyer who specifies paint-shop-appropriate workwear faces: - Chemical exposure controlled (chemical-resistant fabric minimizes absorption) - Paint defects reduced (low-lint fabric minimizes contamination) - Regulatory compliance maintained (chemical exposure monitoring demonstrates due diligence) - Garment service life optimized (wash-durable fabric maintains performance through frequent laundering)
Sourcing approach
How a factory partner can respond
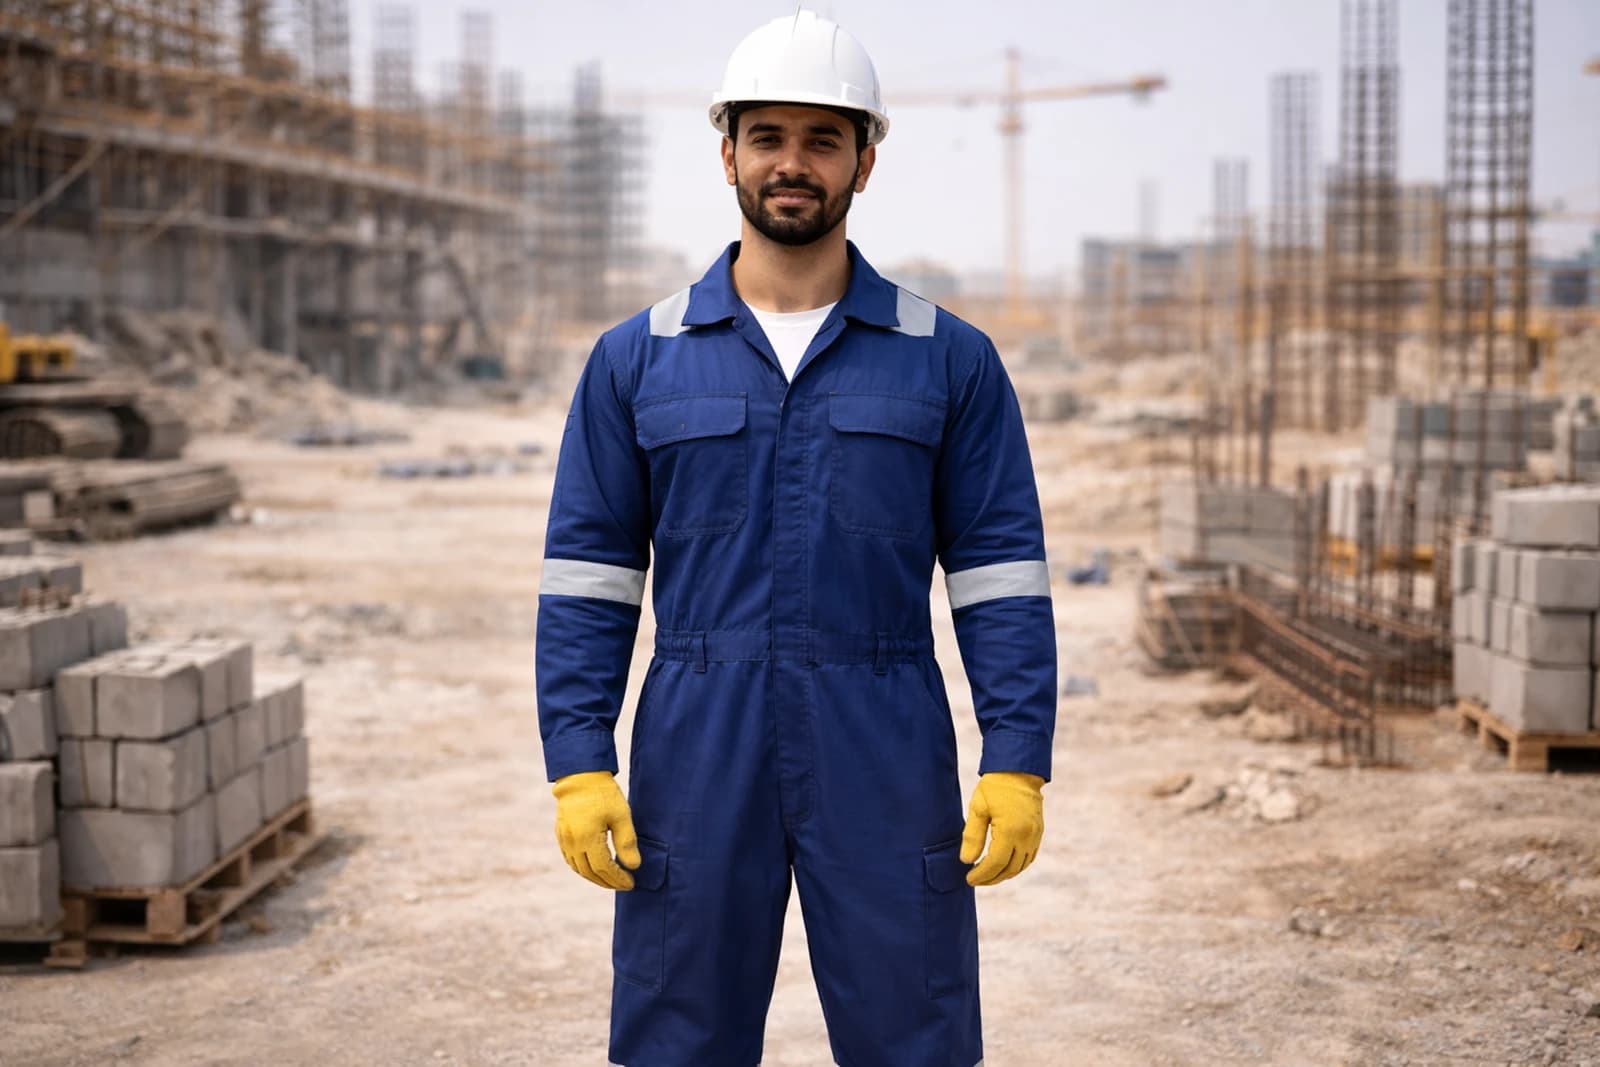
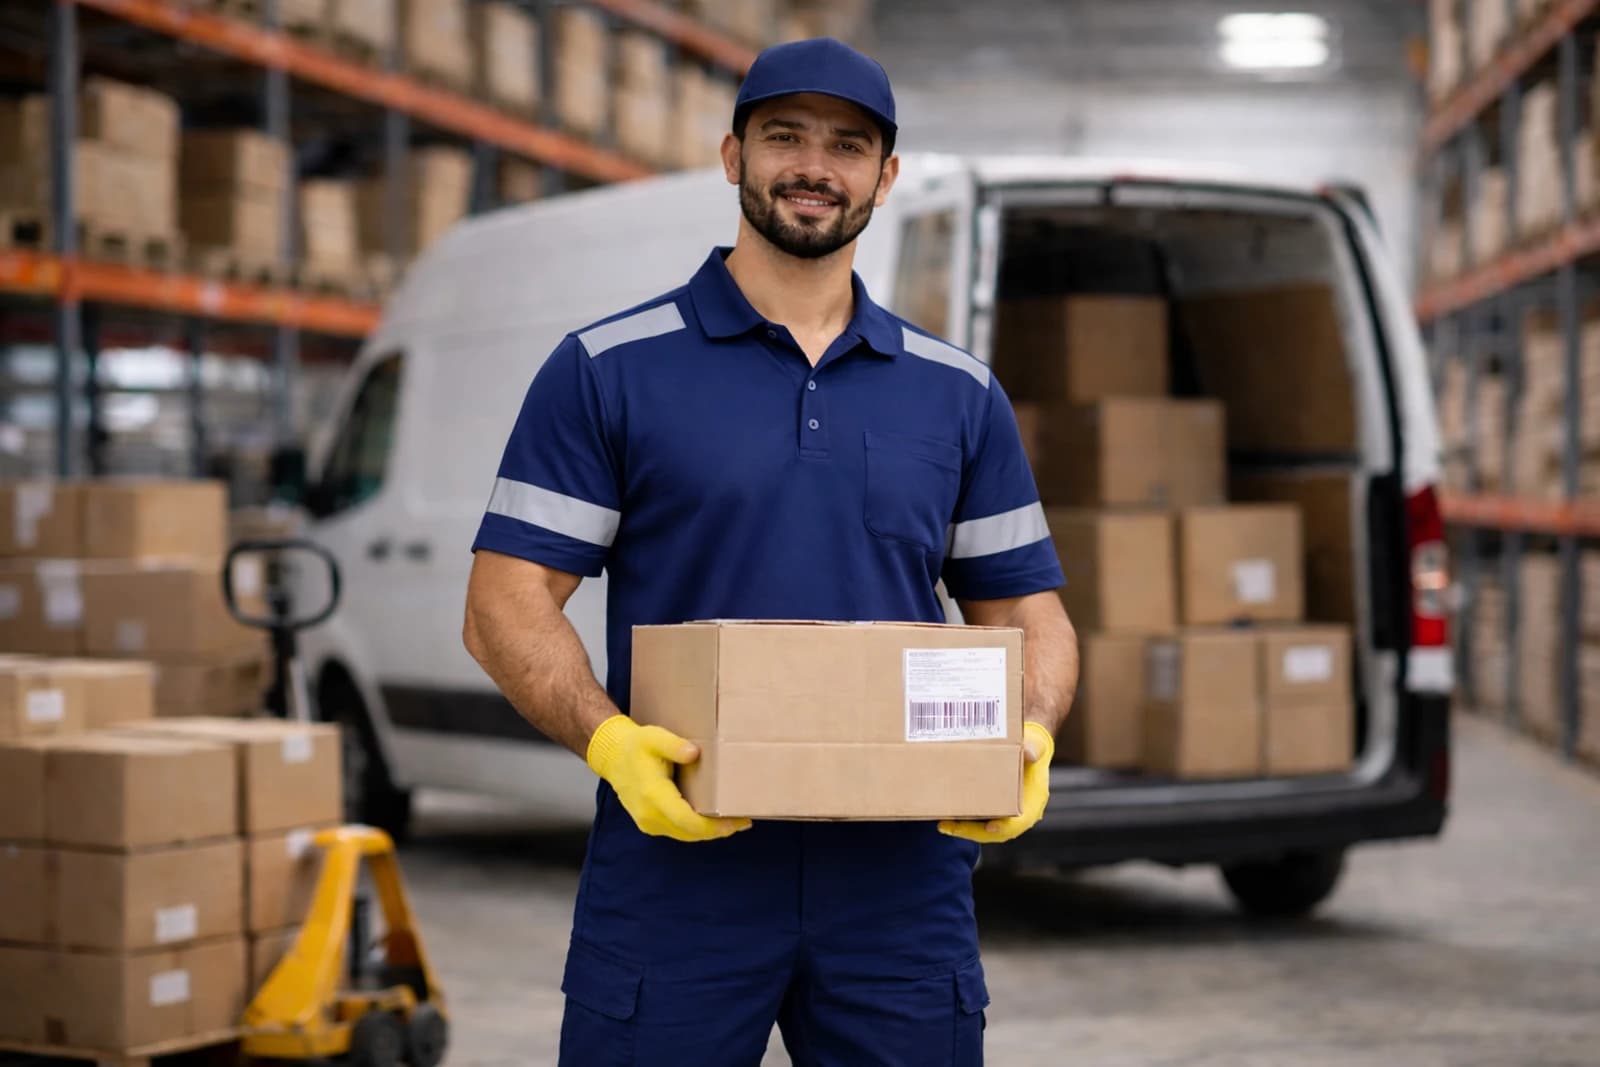
The solution is an automotive paint shop workwear specification that addresses chemical resistance, low-lint performance, zone-based coverage, and wash durability — treating chemical absorption and lint generation as the dual constraints that define paint shop workwear requirements. **Step 1: Specify chemical-resistant fabric that minimizes absorption** For automotive paint shop workwear, specify fabrics that resist chemical absorption and enable effective decontamination: - **Tight-weave polyester or polyester-blend fabric:** specify fabric with a tight weave (minimum 150 gsm) that minimizes chemical absorption. Polyester absorbs less liquid than cotton — solvents and paints remain on fabric surface where they can be removed by laundering, rather than penetrating into fabric fibers. - **Chemical-resistant finish:** specify fabric with a chemical-resistant finish (water-repellent treatment, chemical-barrier coating) that prevents chemicals from penetrating fabric. Chemical-resistant finishes cause liquids to bead up and roll off fabric surface, minimizing absorption. Require supplier testing data confirming that the chemical-resistant finish withstands 25, 50, and 75 wash cycles — topical treatments degrade through laundering, so permanent chemical resistance (integrated into fabric structure) is preferred. - **Smooth fabric surface:** specify fabric with a smooth surface finish that minimizes lint generation. Smooth surfaces don't create loose fibers that shed and contaminate paint. Avoid brushed cotton, fleece-lined fabrics, and textured surfaces that generate lint. - **Wash durability:** require supplier testing data confirming that fabric maintains chemical resistance and low-lint properties after 25, 50, and 75 wash cycles. The testing data proves that garments maintain performance throughout their service life. The fabric specification ensures that garments minimize chemical absorption and lint generation — the dual constraints that define paint shop workwear requirements. **Step 2: Specify garment construction that minimizes lint generation** Specify garment construction that eliminates features that generate lint or trap chemicals: - **Enclosed seams:** specify flat-felled seams or bound seams that enclose raw fabric edges. Enclosed seams eliminate raw edges that shed fibers and trap chemicals. - **Minimal external pockets and components:** specify garments with minimal external pockets, flaps, and loose components. External pockets and flaps create additional surface area that generates lint and traps chemicals. If pockets are required, specify internal pockets accessed through a sealed opening, or specify pockets with smooth, flush closures. - **Covered zippers or snap closures:** specify zippers with fabric flaps that cover the zipper teeth, or specify snap closures that don't generate lint. Metal zippers can corrode when exposed to chemicals, creating additional contamination risk. - **Printed labels or low-lint sewn labels:** specify printed labels or labels that are sewn flat against the garment with low-lint thread. Standard labels shed fibers and create lint contamination. - **No loose components:** specify garments with no drawstrings, loose labels, or dangling components. Loose components trap chemicals and generate lint. The construction specification ensures that garment features don't generate lint or trap chemicals in paint shop operations. **Step 3: Create a zone-based specification that matches garment coverage to each area** Automotive paint shops have distinct zones with different chemical exposure and contamination control requirements. Specify different garments for each zone: - **Paint mixing and preparation areas:** specify full coverall in chemical-resistant, low-lint polyester fabric. The coverall provides full body coverage, minimizing skin exposure to concentrated chemicals. Specify the coverall with enclosed seams, minimal external pockets, covered zippers, and printed labels. Specify the coverall with chemical-resistant finish that withstands frequent laundering. - **Paint application (spray booths):** specify full coverall in chemical-resistant, low-lint polyester fabric. The coverall provides full body coverage, minimizing skin exposure to spray mist and overspray while also minimizing lint generation that can defect wet paint. Specify the coverall with the same construction features as mixing area garments. Specify the coverall in a light color that makes paint overspray visible — visible overspray signals to the worker that the garment needs laundering or replacement. - **Curing and inspection areas:** specify coverall or two-piece suit (shirt and trouser) in chemical-resistant, low-lint polyester fabric. These areas have lower chemical exposure but still require contamination control. Specify the garment with breathable construction for comfort in curing areas where temperatures may be elevated. - **Administrative and support areas:** specify polo shirt and trouser in low-lint polyester fabric. These areas have minimal chemical exposure and contamination control requirements — the polo provides professional appearance without the full coverage needed in paint operations. The zone-based specification matches garment coverage and cost to each area's chemical exposure and contamination control requirements. The buyer doesn't over-specify workwear for administrative areas (paying for full coveralls not needed) and doesn't under-specify workwear for paint operations (creating chemical exposure and paint defect risk). **Step 4: Implement a frequent laundering program with validation** Frequent laundering is required to remove chemical residues and maintain low-lint performance. Implement a laundering program that ensures garments are effectively decontaminated: - **Daily or shift-change laundering:** garments are laundered daily or at shift change to prevent chemical buildup and maintain low-lint performance. Specify wash parameters (water temperature, detergent type, rinse cycles) that remove chemical residues without degrading fabric properties. - **Laundering validation:** test garments after laundering for chemical residues (wipe sampling analyzed by laboratory) and lint generation (lint testing using standardized methods). If chemical residues remain above dermal exposure reference levels after washing, or if lint generation exceeds acceptable thresholds, adjust wash parameters or reduce the replacement interval. - **Post-wash inspection:** garments are inspected after each wash cycle for residual chemical odor, visible chemical stains, and fabric degradation. Garments that fail post-wash inspection are rewashed or removed from service. The laundering program ensures that garments are effectively decontaminated and maintain low-lint performance throughout their service life. **Step 5: Track garment condition and replace based on chemical exposure load** Frequent laundering degrades fabric over time. Track garment condition and replace garments before fabric degradation increases chemical absorption or lint generation: - **Wash cycle tracking:** record the number of wash cycles for each garment. Set a maximum wash cycle limit based on supplier wash durability testing (e.g., replace garments after 50 wash cycles if wash durability testing confirms fabric maintains properties through 50 cycles). - **Periodic fabric inspection:** inspect garments periodically (monthly or quarterly) for fabric degradation — surface roughness, weave loosening, seam degradation, closure damage. Garments that show fabric degradation are removed from service regardless of wash cycle count. - **Chemical exposure tracking:** track chemical exposure events per garment (visible chemical stains, chemical odors that persist after washing). Garments with high chemical exposure loads are removed from service even if they haven't reached the maximum wash cycle limit. The tracking and replacement protocol ensures that garments are replaced before fabric degradation increases chemical absorption or lint generation — maintaining performance throughout garment service life. **Step 6: Address garment removal as a chemical exposure event** When workers remove chemically contaminated garments, they contact the contaminated fabric surface. Chemical residues on the outer surface transfer to skin through handling. If workers then touch their face, eat, or handle personal items without hand washing, they create a secondary exposure pathway. Implement controls: - **Removal procedure:** train workers to remove garments without contacting the outer surface (roll garment inward, avoid shaking garments that release lint). - **Gloves for removal:** require workers to wear disposable gloves during garment removal if the garment is known or suspected to be chemically contaminated. - **Hand hygiene:** enforce hand washing or hand sanitizing immediately after garment removal, before touching personal items, eating, or using phones. - **Contaminated garment handling:** place removed garments directly into designated laundry bags without intermediate handling. Do not store contaminated garments in lockers or personal areas. The removal controls prevent secondary exposure from chemically contaminated garments — the exposure pathway that occurs when workers handle contaminated fabric during removal. **Recommended garments for automotive paint shop workwear:** - **Industrial coverall-pro** — specify the coverall for paint mixing, preparation, and spray booth areas where chemical exposure is highest and contamination control is critical. The coverall's full-body coverage minimizes skin exposure to solvents, paints, and hardeners. Specify the coverall in chemical-resistant, low-lint polyester fabric with a tight weave, smooth surface finish, and chemical-resistant finish that withstands frequent laundering. Specify the coverall with enclosed seams, minimal external pockets, covered zippers, and printed labels. Specify the coverall with wash durability testing data confirming that fabric maintains chemical resistance and low-lint properties after 50 wash cycles. Specify the coverall in a light color that makes paint overspray visible. The coverall's chemical-resistant fabric, low-lint construction, and wash durability make it suitable for automotive paint shop operations where chemical exposure and paint defect prevention are critical. - **Logistics polo uniform** — specify the polo for administrative and support areas where chemical exposure is minimal and full coveralls are not required. The polo's polyester-based fabric provides low-lint performance and professional appearance for customer-facing areas (showrooms, delivery areas). Specify the polo in a smooth, tight-weave fabric with minimal external components and printed labels. Specify the polo in company-branded colors for professional appearance. The polo's low-lint fabric, comfort, and professional appearance make it suitable for administrative areas in automotive paint facilities where appearance and minimal contamination risk are required.
Recommended Products
Products that fit this use case
Industrial Workwear
Industrial Coverall Pro
Hard-wearing one-piece coverall for plant, maintenance, and heavy-duty operations.
Logistics Uniform
Logistics Polo Uniform
Breathable uniform polo for warehouse, delivery, and last-mile teams.