Write a Workwear Specification That Suppliers Cannot Misinterpret
Most workwear specifications read like a wish list: breathable fabric, durable construction, comfortable fit, good value. Suppliers read the same specification and produce a garment that meets none of those terms because none of them are measurable. The result is a sample that looks acceptable on paper but fails in wear, a bulk order that does not match the sample, or a delivery that technically meets the specification but does not meet the buyer's actual need. This article covers the specific, measurable criteria that replace vague specification language, the structure that prevents suppliers from filling gaps with their own assumptions, and the approval sequence that catches misinterpretation before bulk production commits.
Buyer context
What procurement teams run into
Workwear buyers issue specifications to suppliers expecting that the supplier will produce garments matching the buyer's intent. In practice, specifications contain vague, unmeasurable, or incomplete language that allows suppliers to interpret requirements in ways that do not match the buyer's actual need. The mechanism: **1. Vague fabric descriptions allow supplier interpretation** Specifications that state "breathable fabric," "durable construction," or "comfortable fit" do not define measurable criteria. A supplier can interpret "breathable" as any fabric with moderate air permeability — including a 150 GSM lightweight polyester that meets the buyer's word but not the buyer's need for a 220 GSM fabric with moisture-wicking treatment for 38°C outdoor work. The supplier produces a garment that is technically "breathable" but does not perform in the actual work environment. The root cause: the specification uses qualitative adjectives instead of quantitative parameters. "Breathable" is not a test result. "Durable" is not a fabric weight or abrasion cycle count. "Comfortable" is not a moisture vapor transmission rate or a fabric hand-feel standard. **2. Missing performance thresholds allow minimum compliance** Specifications that state fabric requirements without performance thresholds allow suppliers to meet the minimum possible standard. A specification that states "fabric must resist abrasion" without defining the abrasion test method and minimum cycle count allows the supplier to select a fabric that passes a basic abrasion test at 5,000 cycles — while the buyer's actual need is a fabric that survives 25,000 cycles in the worker's knee and seat areas. The supplier's garment meets the specification but fails in the field. The root cause: the specification does not define the performance threshold that matches the actual work environment. Without a threshold, the supplier optimizes for cost — selecting the minimum fabric that meets the specification's words but not the buyer's intent. **3. Incomplete design descriptions allow supplier assumptions** Specifications that describe garment types without complete design details allow suppliers to fill gaps with their own assumptions. A specification that states "coverall with zip front" does not define zipper type (metal or plastic), zipper gauge (#5 or #10), zipper coverage (exposed or covered with storm flap), zipper stop position (chest or waist), or reinforcement at zipper stress points. The supplier selects the lowest-cost zipper that fits the description — a #5 plastic zipper with no storm flap — while the buyer's actual need is a #10 metal zipper with a storm flap for heavy industrial use. The root cause: the specification does not define design details at the level of specificity needed for production. The supplier fills gaps with cost-optimized defaults that do not match the buyer's intent. **4. No reference garment or benchmark allows interpretation drift** Specifications that do not include a reference garment, benchmark sample, or visual standard allow each party to interpret the specification differently. The buyer envisions a garment based on their experience and mental image. The supplier envisions a garment based on their standard product range and production capabilities. The two visions do not match — but neither party discovers the gap until the sample arrives, by which time production tooling may already be committed. The root cause: the specification relies on text description alone, without a physical or visual reference that anchors interpretation to a specific garment. **5. Approval sequence does not catch misinterpretation before bulk** Specifications that move directly from text description to bulk production — without a structured sampling sequence that tests interpretation at each stage — allow misinterpretation to compound. The supplier produces a bulk order based on their interpretation of the specification. The buyer receives the bulk order and discovers that the garment does not match their intent. The cost of correction — re-production, delay, rejection — falls on both parties. The root cause: the approval sequence does not include intermediate checkpoints that test the supplier's interpretation before bulk production commits. **6. The cost of misinterpretation** The buyer who issues a vague specification faces: - Samples that look acceptable but fail in wear — the garment meets the specification's words but not the buyer's actual performance need - Bulk orders that do not match the sample — the supplier's production interpretation differs from the sample approval - Garments that technically meet the specification but do not meet the buyer's need — the supplier optimized for cost within the specification's gaps - Rework, rejection, or replacement costs — the cost of correcting misinterpretation after bulk production - Delayed delivery — re-production or negotiation extends the delivery timeline - Relationship friction — the buyer and supplier disagree about whether the garment meets the specification, creating dispute
Sourcing approach
How a factory partner can respond
The solution is a workwear specification structured around specific, measurable, and complete criteria — replacing vague language with quantitative parameters, defining performance thresholds that match the actual work environment, and building an approval sequence that catches misinterpretation before bulk production. **Step 1: Replace qualitative adjectives with quantitative parameters** Every fabric and performance requirement in the specification must be stated as a measurable parameter with a test method: - Instead of "breathable fabric": specify "fabric air permeability ≥ 40 L/m²/s tested per ISO 9237" - Instead of "durable fabric": specify "fabric weight 240–260 GSM, abrasion resistance ≥ 25,000 cycles tested per ISO 12947-2" - Instead of "comfortable fit": specify "garment dimensions per size chart [attached], with ≤ 3% shrinkage after 5 wash cycles at 60°C tested per ISO 6330" - Instead of "colorfast fabric": specify "color fastness to washing ≥ grade 4, color fastness to light ≥ grade 5, tested per ISO 105" - Instead of "strong seams": specify "seam strength ≥ 250 N tested per ISO 13935-1" Each parameter must include: the numeric value, the test method, and the minimum acceptable result. The supplier cannot misinterpret a numeric parameter — the fabric either meets the threshold or it does not. **Step 2: Define performance thresholds that match the actual work environment** Performance thresholds must be derived from the actual work environment, not from generic industry norms. Before writing the specification, document: - Work environment conditions: temperature range, humidity, UV exposure, chemical exposure, abrasion sources - Work activities: physical demands, movement patterns, contact surfaces, tool use - Wash conditions: wash frequency, wash temperature, detergent type, drying method - Required garment life: target replacement cycle in months or wash cycles Use this data to set performance thresholds. For example: - Workers in 38°C outdoor conditions with heavy sweat exposure: specify moisture vapor transmission rate ≥ 8,000 g/m²/24h (high breathability for heat dissipation) - Workers with knee contact on concrete surfaces: specify abrasion resistance ≥ 40,000 cycles (heavy abrasion for knee durability) - Garments washed daily at 60°C: specify shrinkage ≤ 3% after 50 wash cycles at 60°C (high wash durability for daily industrial laundering) The threshold must match the actual need — not a generic standard that may be too low for the work environment. **Step 3: Define complete design details at production-level specificity** Every design element must be specified at the level of detail needed for production — not at the level of a general description. The specification must include: - **Garment type and style:** coverall, two-piece set, jacket, polo — with style reference drawing or technical sketch - **Fabric:** fiber content (% polyester, % cotton, or specialty fiber), fabric weight (GSM), weave type (twill, plain, ripstop), finish (DWR, moisture-wicking, FR treatment) - **Closures:** zipper type (metal/plastic), zipper gauge (#5, #10), zipper coverage (exposed/covered), zipper length, snap type and spacing, button type and count - **Reinforcement:** double-layer knees, double-layer seat, reinforced cuffs, bar-tack at stress points — with specific location and reinforcement method - **Pockets:** pocket type (chest, side, cargo, internal), pocket dimensions, pocket closure (flap, zipper, snap), pocket reinforcement - **Seams:** seam type (felled, bound, overlocked), seam allowance, stitch density (stitches per cm) - **Cuffs and collar:** cuff type (elastic, snap-adjustable, knit), collar type (mandarin, turnover, knit) - **Reflective elements:** tape width, tape placement, tape type (stitched, heat-bonded), compliance standard (EN ISO 20471 or equivalent) - **Sizing:** size range, size chart with body dimensions and garment dimensions, grading rules between sizes - **Labels and markings:** care label content, size label placement, logo placement and method (embroidery, print, woven label) - **Packing:** folding method, poly bag specifications, carton markings, size ratio per carton Each design element must be specific enough that a production factory can produce the garment without making assumptions. If the specification does not define a detail, the supplier will choose — and their choice will optimize for their cost, not the buyer's need. **Step 4: Include a reference garment or benchmark sample** Where possible, include a physical reference garment or benchmark sample with the specification. The reference garment anchors the specification to a real, tangible product — eliminating interpretation drift from text description alone. - If the buyer has an existing garment that performs well: send the garment as a reference, with a note specifying which elements to match (fabric, design, fit) and which elements to change (add pockets, change color, modify sizing). - If the buyer does not have a reference garment: request the supplier to produce a benchmark sample based on the specification before bulk production. Approve the benchmark sample as the physical standard against which bulk production is measured. - Include photographs of the reference garment or benchmark sample with the specification — front view, back view, detail views of closures, pockets, seams, and reinforcement. The reference garment or benchmark sample becomes the physical standard that both parties agree represents the specification's intent. **Step 5: Build a structured sampling sequence with approval gates** The sampling sequence must include intermediate checkpoints that test the supplier's interpretation before bulk production commits: - **Stage 1: Fabric submission and testing.** The supplier submits fabric swatches with test reports confirming that the fabric meets all specified parameters (weight, fiber content, air permeability, abrasion resistance, color fastness, shrinkage). The buyer reviews test reports and approves the fabric before garment production begins. If the fabric does not meet parameters, the supplier sources alternative fabric and resubmits. - **Stage 2: Pre-production sample (PP sample).** The supplier produces one complete garment in the approved fabric, in the buyer's middle size (e.g., size L). The PP sample tests the supplier's interpretation of design details — closure selection, pocket placement, seam construction, reinforcement method, labeling, and overall workmanship. The buyer reviews the PP sample against the specification and reference garment. If the PP sample does not match, the supplier corrects and resubmits. The buyer approves the PP sample in writing before bulk production begins. - **Stage 3: Size set sample.** The supplier produces one garment in each size of the size range (S, M, L, XL, XXL). The size set tests the supplier's grading — whether the garment dimensions increase proportionally across sizes and whether fit is maintained. The buyer measures each garment against the size chart and confirms that grading is correct. If grading is incorrect, the supplier adjusts the pattern and resubmits. - **Stage 4: Pre-shipment sample (PS sample).** The supplier produces a sample from the bulk production run — a garment that represents the actual bulk quality. The buyer reviews the PS sample against the approved PP sample and size set. If the PS sample matches, the buyer authorizes shipment. If the PS sample does not match, the buyer rejects the bulk or requires correction before shipment. Each stage is an approval gate — bulk production does not proceed until the buyer approves the current stage in writing. The sequence catches misinterpretation at the earliest possible point, before bulk production commits cost and timeline. **Step 6: Specify inspection and acceptance criteria** The specification must define how the buyer will inspect and accept the bulk delivery: - **Inspection standard:** specify the inspection method (e.g., ANSI/ASQ Z1.4 or ISO 2859-1) and acceptable quality level (AQL) for defects (e.g., AQL 2.5 for major defects, AQL 4.0 for minor defects). - **Measurement tolerance:** specify the allowable deviation from the size chart (e.g., ± 1.5 cm on body dimensions). Garments outside tolerance are rejected. - **Defect classification:** define major defects (fabric damage, incorrect size, wrong color, missing closures, seam failure) and minor defects (loose thread, slight color variation, labeling error). Major defects result in rejection. Minor defects are counted against the AQL. - **Inspection timing:** specify whether inspection occurs pre-shipment (at the supplier's factory) or upon receipt (at the buyer's warehouse). Pre-shipment inspection catches defects before the garment ships, reducing return logistics cost. The inspection criteria give both parties a clear, agreed standard for acceptance — eliminating dispute about whether the bulk delivery meets the specification. **Recommended garments for specification-driven procurement:** - **Industrial coverall-pro** — use as a reference garment when specifying coveralls for heavy industrial use. The coverall's design details — #10 metal zipper with storm flap, double-layer knees with reinforcement, bar-tack at stress points, bound seams, snap-adjustable cuffs — provide a benchmark for specification language. Specify the coverall with quantitative fabric parameters (weight, fiber content, abrasion resistance, shrinkage) and complete design details (closure type, pocket configuration, reinforcement placement, seam construction). - **Logistics polo uniform** — use as a reference garment when specifying polo shirts for general site use. The polo's design details — collar construction, placket closure, sleeve hem, side vents, logo placement — provide a benchmark for specification language. Specify the polo with quantitative fabric parameters (weight, fiber content, moisture-wicking rate, color fastness) and complete design details (collar type, placket type, hem type, labeling).
Recommended Products
Products that fit this use case
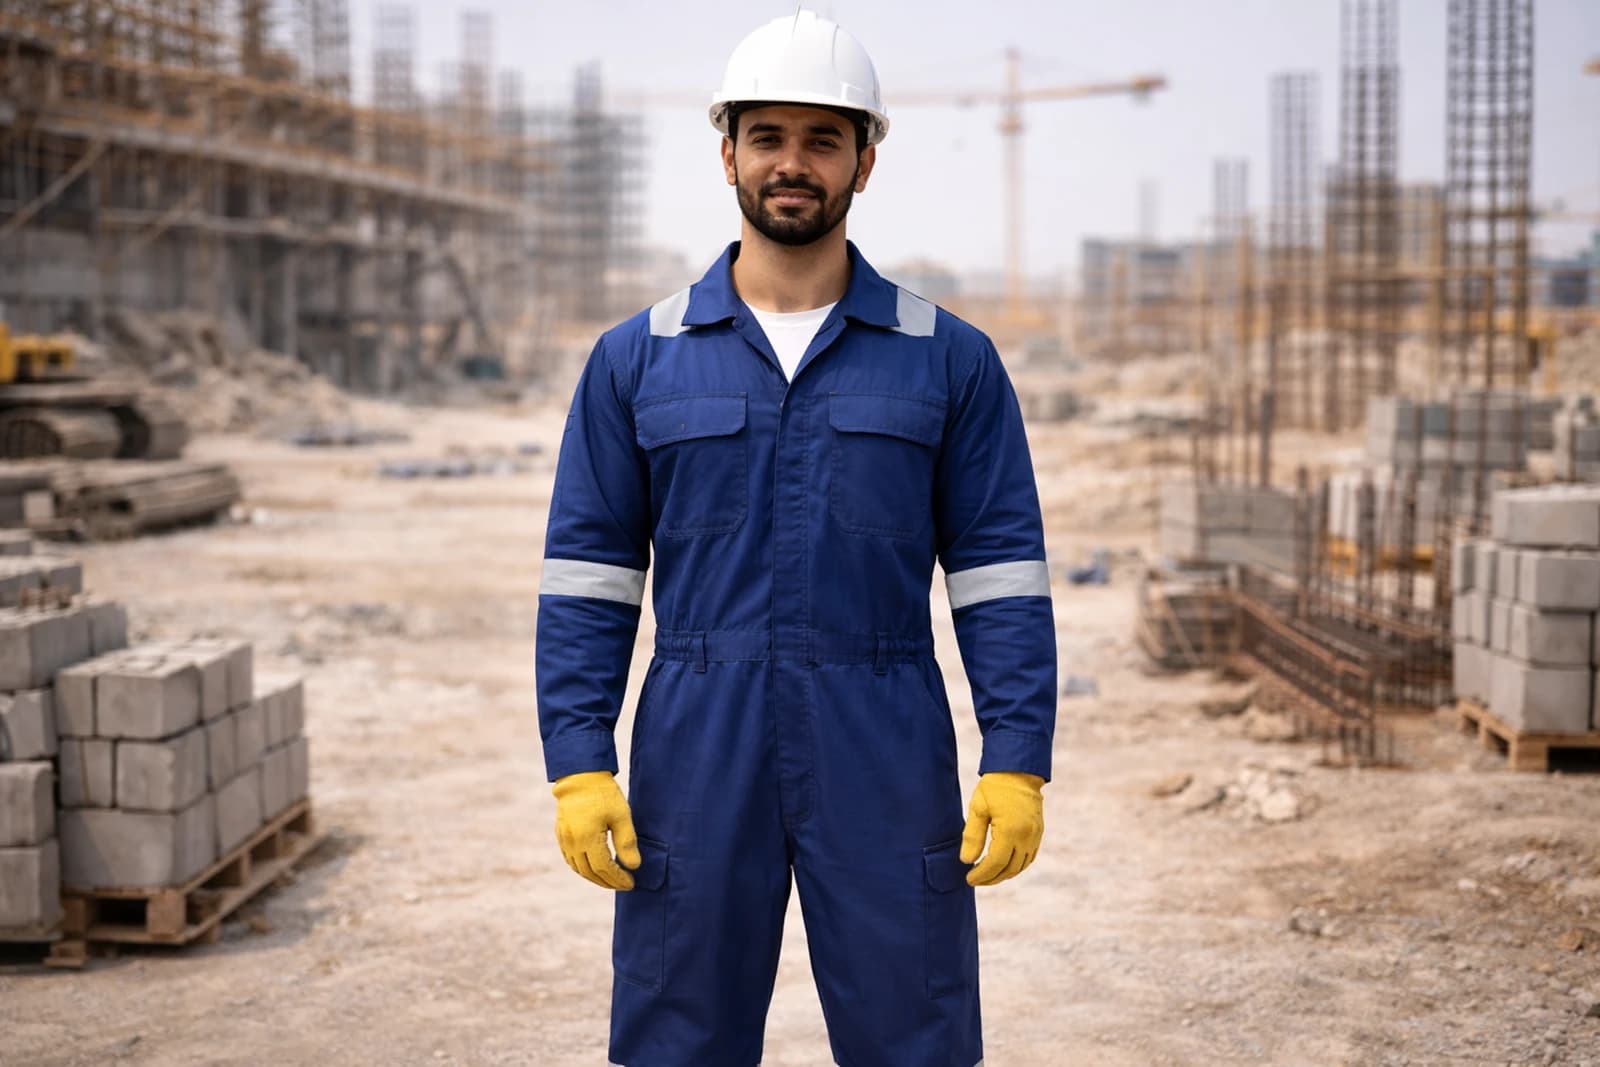
Industrial Workwear
Industrial Coverall Pro
Hard-wearing one-piece coverall for plant, maintenance, and heavy-duty operations.
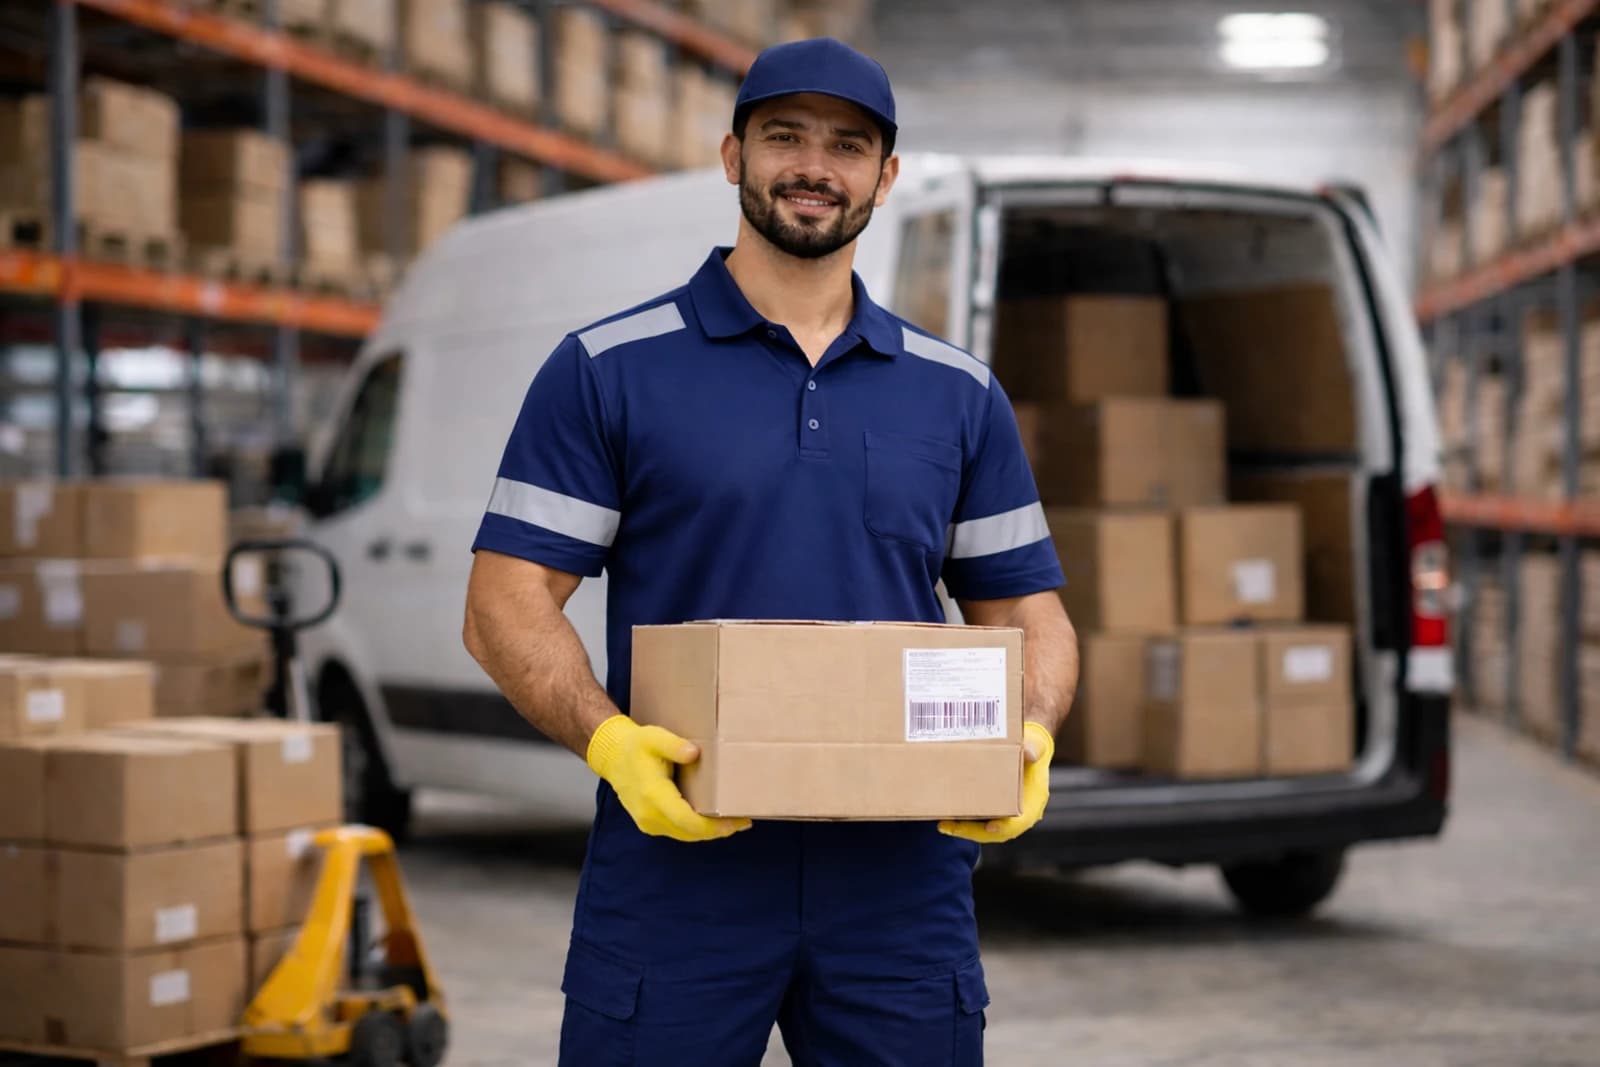
Logistics Uniform
Logistics Polo Uniform
Breathable uniform polo for warehouse, delivery, and last-mile teams.